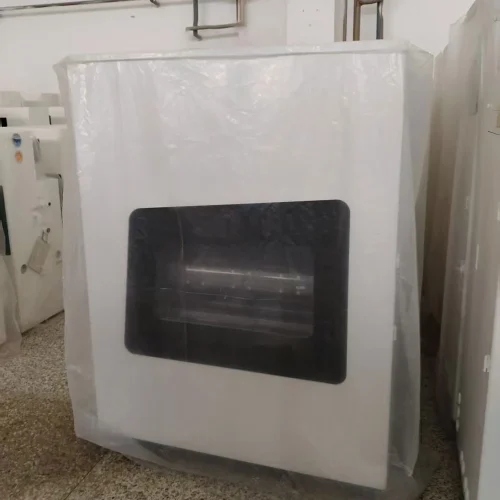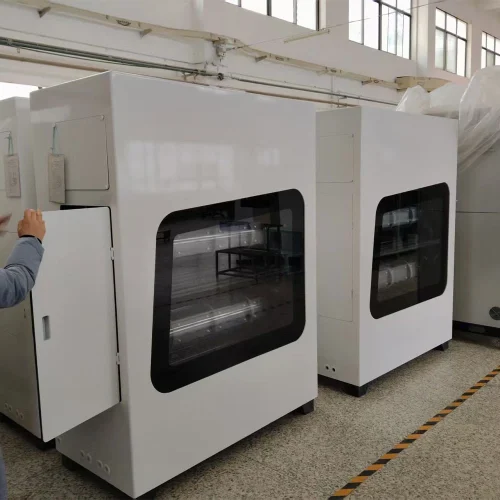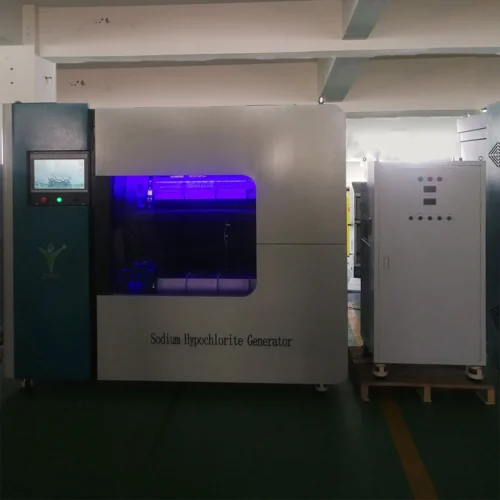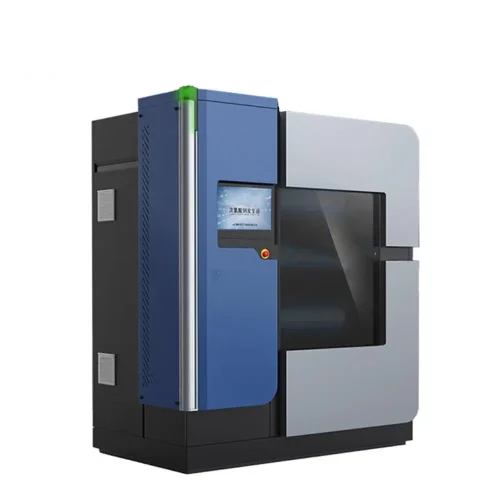


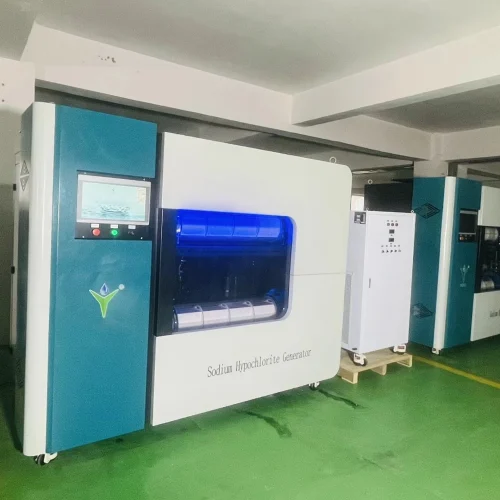
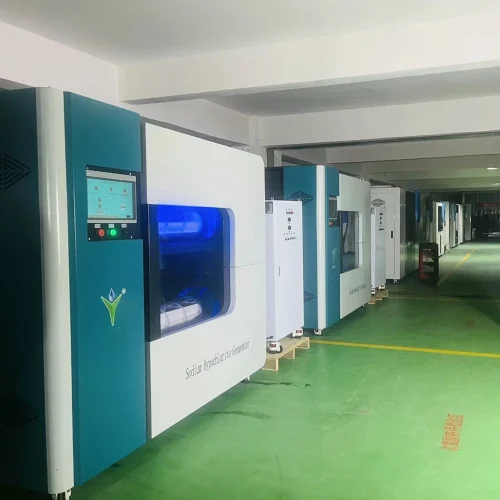
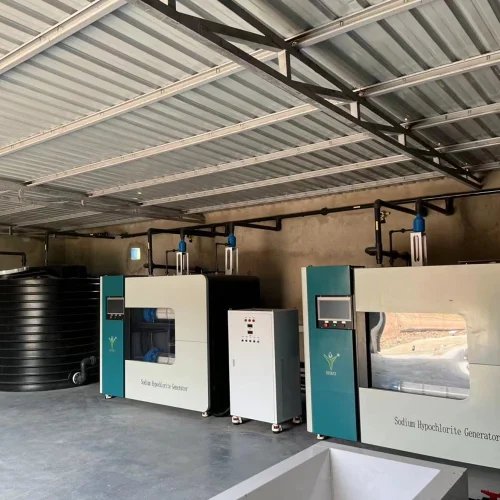
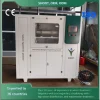
In the critical field of municipal water treatment, safety, reliability, and efficiency are paramount. Large-scale water purification plants face the immense challenge of delivering clean, safe drinking water to millions of people. Addressing this challenge head-on is the advanced SHT-10000G Sodium Hypochlorite Generator, a state-of-the-art solution designed for high-capacity water disinfection. This robust system represents the pinnacle of modern electrochemical technology, offering unparalleled performance for large waterworks. Its successful application in over 30 countries and regions stands as a testament to its global trust and superior capabilities. Furthermore, with innovative features like network connectivity for remote monitoring, the SHT-10000G is setting a new standard for operational intelligence and convenience in the water treatment industry.
1. The Core of Modern Disinfection: On-Site Generation
Traditionally, water treatment facilities have relied on the transport and storage of bulk chlorine gas or commercial sodium hypochlorite solutions. These methods, while effective, come with significant risks. Chlorine gas is highly toxic and poses a severe safety hazard in the event of a leak. Commercial hypochlorite solutions are corrosive, degrade over time, and present their own set of handling and storage challenges.
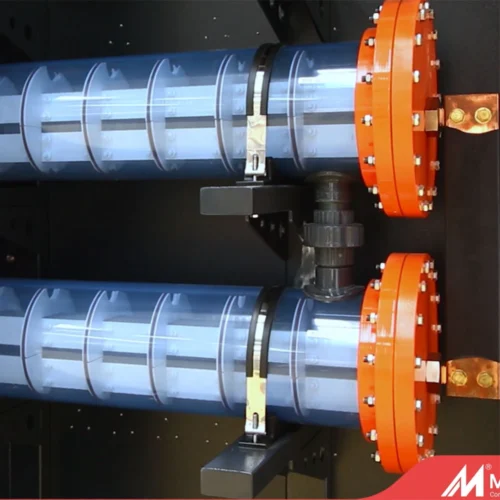
The SHT-10000G sodium hypochlorite generator elegantly circumvents these issues through on-site generation. This process involves the electrolysis of a simple brine solution—a mixture of common salt and softened water. The generator passes a controlled electrical current through the brine in an electrolytic cell, producing a fresh, stable, and low-concentration (typically less than 1%) sodium hypochlorite solution. This method is inherently safer. It completely eliminates the need to transport and store hazardous chemicals. Consequently, it drastically reduces risks to both plant personnel and the surrounding community.
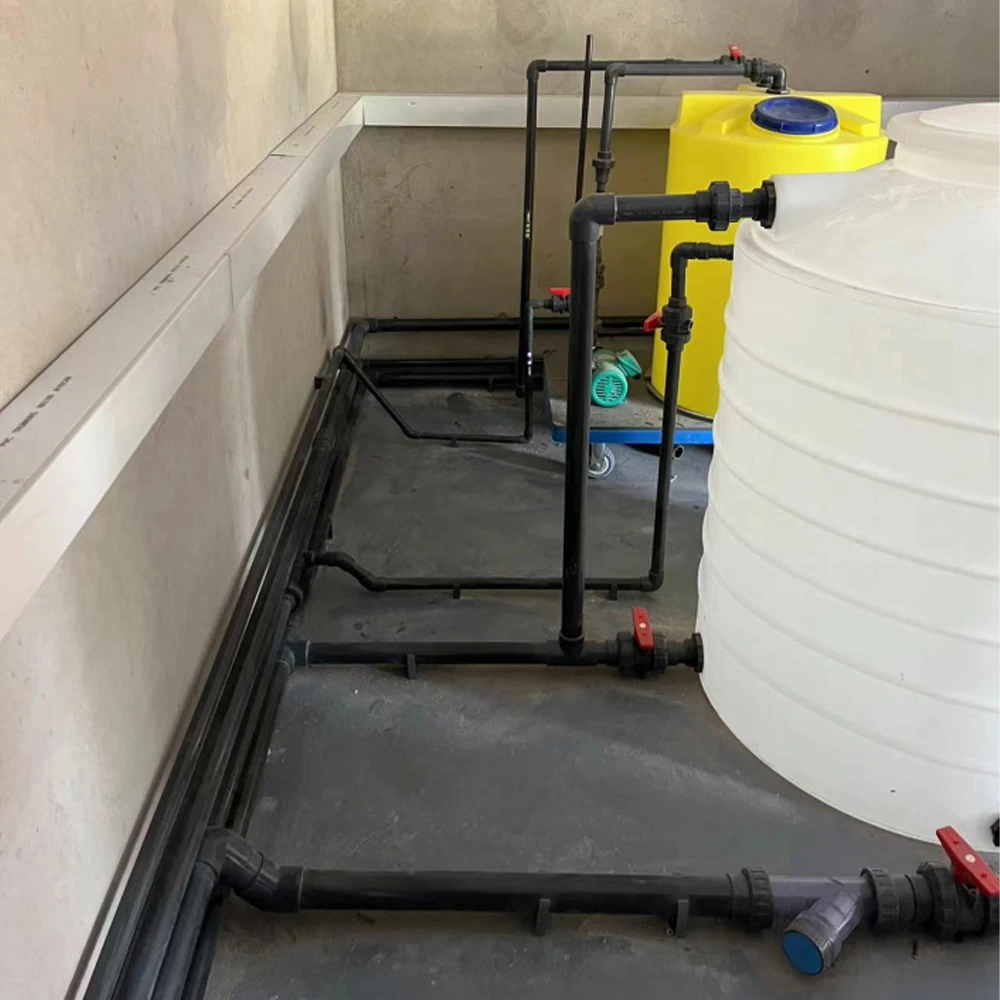
2. Sodium hypochlorite generator parameter
| Product name | SHT-10000G |
|---|---|
| Effective chlorine yield | 10000g/H |
| Concentration | 6-8g/L(6000-8000ppm) |
| Power | 60KW |
| Salt consumption | 3.2KG/KG |
| Size | 2600*900*2000mm |
| Voltage | 380V/50hz |
3. Unmatched Performance: The SHT-10000G Advantage
Designed specifically for large-scale applications, the SHT-10000G boasts an impressive production capacity, capable of generating up to 10,000 grams of available chlorine per hour. This substantial output ensures that even the most demanding water treatment plants can meet their disinfection needs consistently and without interruption.
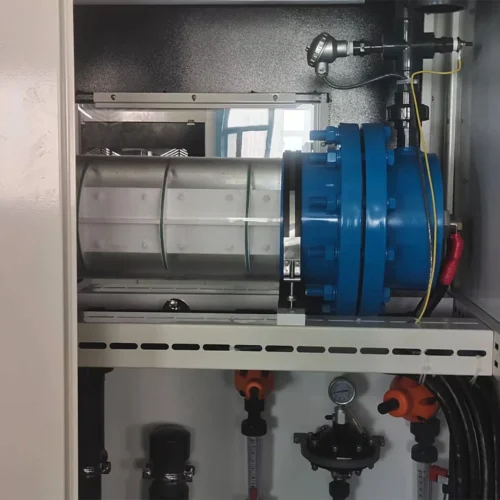
1. At the heart of the SHT-10000G are high-performance electrolytic cells. These cells are constructed from durable, corrosion-resistant materials like titanium, coated with precious metal oxides. This advanced construction not only ensures a long operational lifespan but also maximizes the efficiency of the electrolytic process. The result is lower salt and power consumption per unit of chlorine produced, leading to significant operational cost savings over the system’s lifetime.
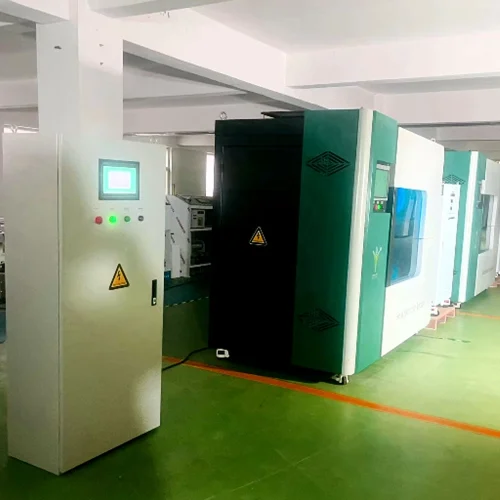
Moreover, the entire system is engineered for reliability. It features a modular design that simplifies maintenance and allows for scalability. Redundant components and automated control systems ensure continuous operation, providing a dependable supply of disinfectant around the clock.
2. A Global Footprint: Trusted Worldwide
The adoption of the SHT-10000G across more than 30 countries and regions is a powerful endorsement of its performance and reliability. From the bustling metropolitan centers of Asia to the growing communities in South America and the established municipalities of Europe, this system has proven its adaptability and effectiveness in a wide range of operational environments.
This global success can be attributed to several key factors. First, the system’s ability to operate effectively in diverse climates and under varying water quality conditions makes it a versatile solution. Second, its compliance with international safety and quality standards provides assurance to water authorities worldwide. Finally, a strong global network of service and support ensures that operators have access to technical assistance whenever needed, fostering long-term partnerships built on trust and reliability. Case studies from these international applications consistently highlight a significant reduction in disinfection by-products, improved water quality, and enhanced operational safety.
3. The Power of Connectivity: Remote Monitoring and Intelligent Operation
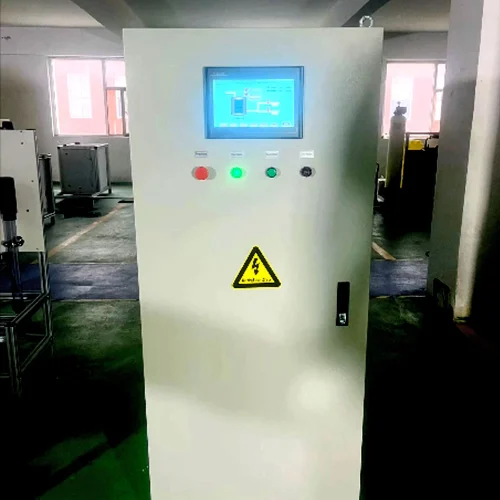
A standout feature of the SHT-10000G is its advanced remote monitoring capability. Equipped with a network port, the system can be seamlessly integrated into a plant’s existing Supervisory Control and Data Acquisition (SCADA) system or accessed through a dedicated web-based portal. This connectivity transforms how the system is managed.
Plant operators and engineers can now monitor key performance indicators from a central control room, a laptop, or even a mobile device. Real-time data on chlorine production, brine concentration, power consumption, and system diagnostics are available at their fingertips. This constant stream of information allows for proactive maintenance and swift troubleshooting. For instance, the system can automatically send alerts via email or SMS if it detects an operational anomaly, such as a drop in brine level or a fluctuation in power supply.
This level of remote oversight is invaluable for large waterworks, which often manage multiple facilities spread across a wide geographical area. It reduces the need for constant on-site supervision, optimizing staffing levels and reducing operational costs. More importantly, it enhances the overall reliability of the water treatment process, ensuring that any potential issues are identify and address before they can impact water quality.

4. Key Advantages Summarized: Why Choose the SHT-10000G?
The benefits of implementing the SHT-10000G sodium hypochlorite generator in a large-scale water treatment facility are numerous and compelling.
1. Enhanced Safety: By generating disinfectant on-site, the system eliminates the risks associated with handling and also storing hazardous chlorine gas or bulk hypochlorite. This creates a safer working environment for employees and provides greater peace of mind for the community.
2. Cost-Effectiveness: The use of common salt and water as raw materials, combined with high energy efficiency, results in a low cost of disinfectant production. The long lifespan of the system components and reduced maintenance requirements further contribute to a lower total cost of ownership.
3. Superior Water Quality: The fresh sodium hypochlorite solution produced by the SHT-10000G is highly effective in neutralizing a broad spectrum of pathogens. Because the solution is freshly made, it has a consistent concentration and does not suffer from the degradation issues common with commercial hypochlorite. This leads to more stable and reliable disinfection.
4. Operational Simplicity: The system is fully automated, with user-friendly controls and a straightforward operating procedure. The integration of remote monitoring further simplifies management, allowing for efficient and effective oversight.
5. Environmental Responsibility: The on-site generation process has a smaller environmental footprint compared to the transportation of bulk chemicals. The system’s high efficiency also minimizes energy consumption, contributing to the overall sustainability of the water treatment plant.

5. A Trusted Partner in Over 30 Countries

FAQ
1. Is on-site generation safer than liquid chlorine?
Yes! No toxic gas storage or transport risks. The system produces only what you need at the same time.
2. What’s the maintenance requirement?
Minimal. Regular cell cleaning and also salt refills. Automated alerts simplify upkeep.
3. How to handle maintenance?
Automated alerts guide servicing.
Factory advantage
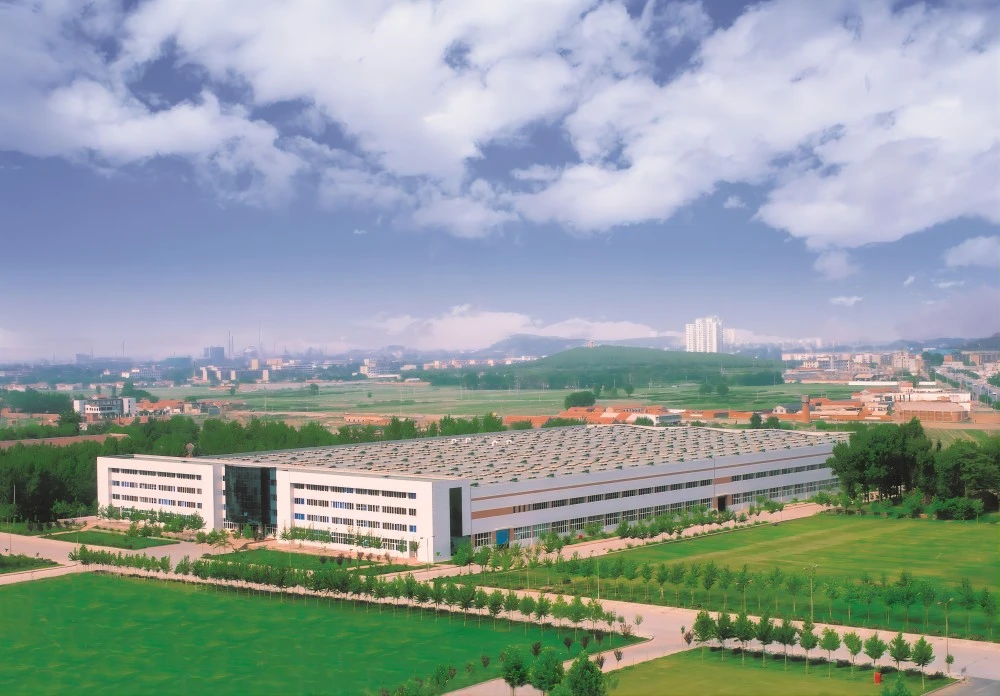
We have R&D centers, production centers, data centers and marketing centers. It is committe to providing technical support and innovative applications for improving public health security. Since its establishment, the company has obtained 12 invention patents and environmental management system certification. The company also has more than 30 test reports, covering surface and other different concentration detection projects. The series products sell well all over the country, and exported to such as Thailand, Malaysia, Cambodia, Brazil, South Africa, South America and other more than 20 countries and regions. The company has a perfect product sales and service system. To meet the needs of different customers with more professional services. So that to provide the best products and services for public health!
Customer feedback