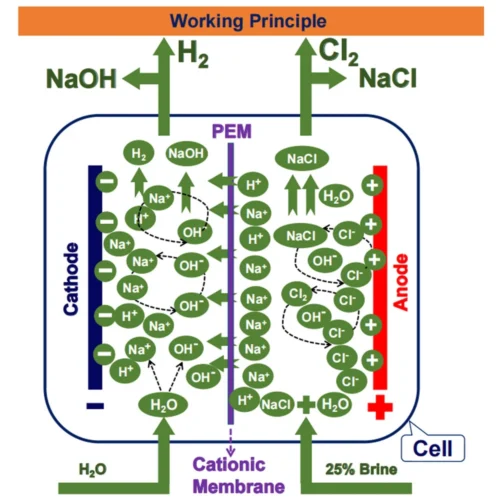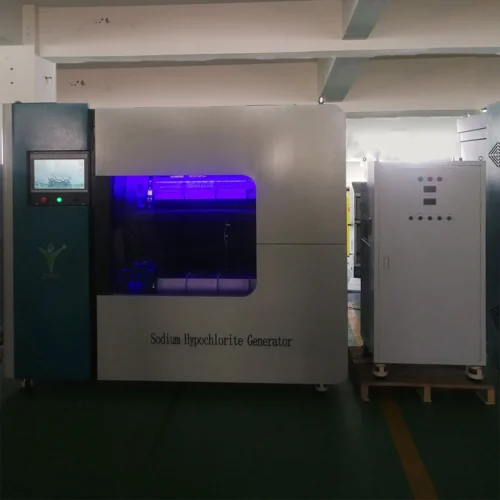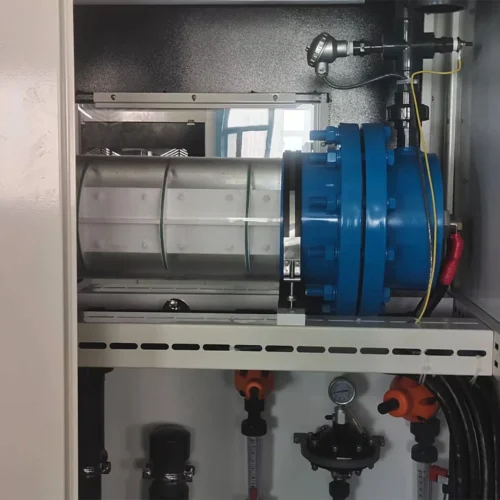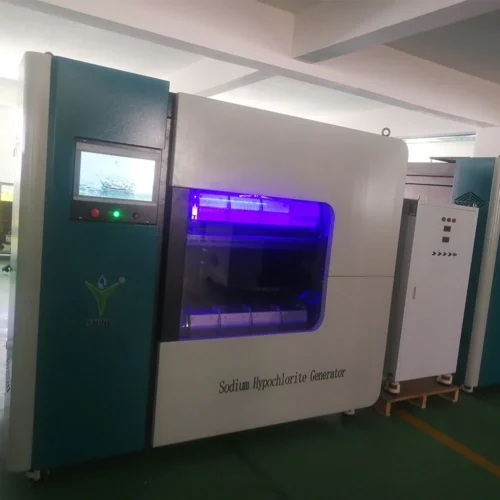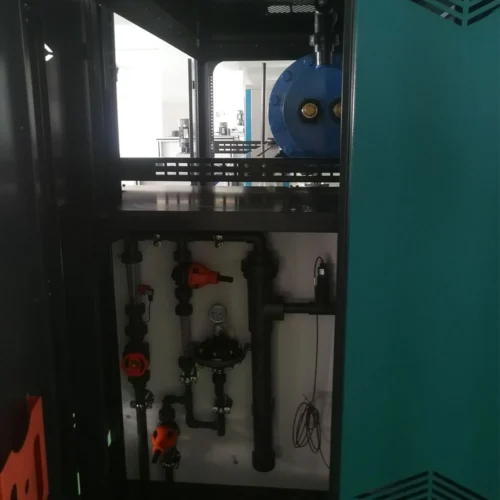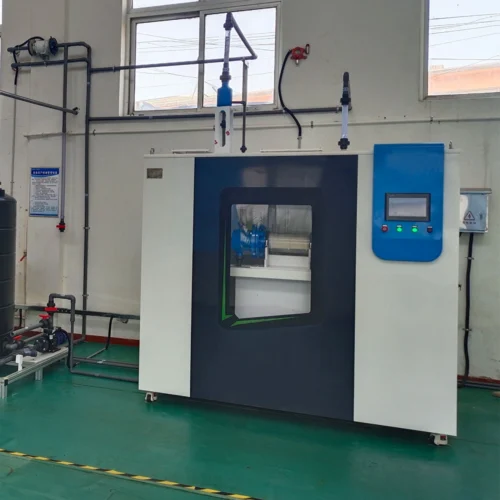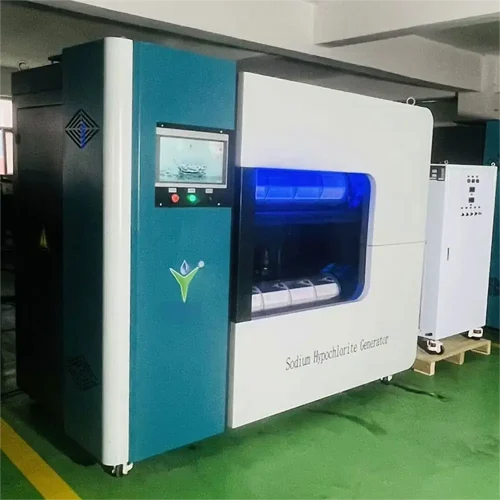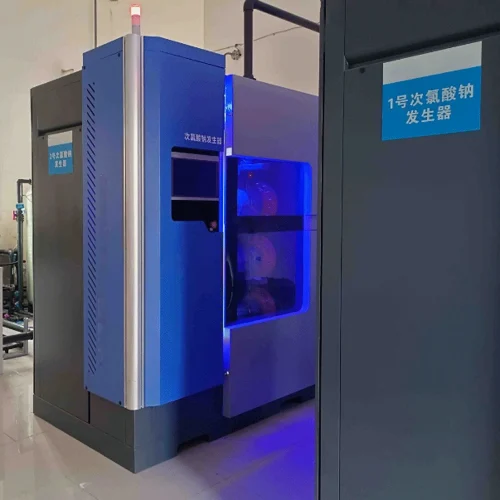


In the demanding world of industrial processing, the efficiency and reliability of your cooling water systems are paramount. However, traditional chemical treatment methods often introduce a host of challenges. From the significant safety risks associated with handling hazardous chemicals to the logistical complexities of transportation and storage, and the ever-present issue of inconsistent dosing, maintaining optimal water quality can be a constant struggle. Furthermore, these conventional approaches can lead to unpredictable operational costs and a substantial environmental footprint.
1. The SHT-500G: A Paradigm Shift in Product Advantage
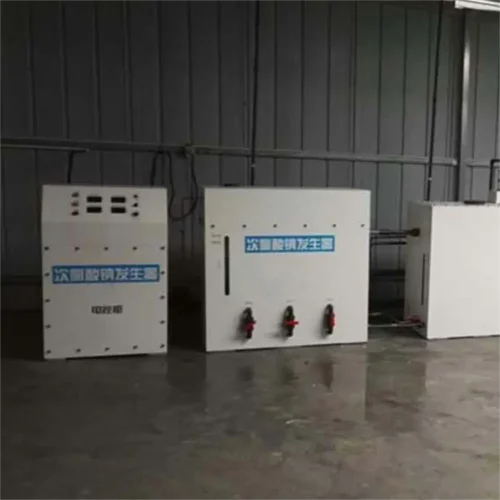
SHT-500G is meticulously engineered to deliver a multitude of benefits that directly address the pain points of modern industrial facilities. Its design and also functionality are centered around providing a superior alternative to traditional water treatment methods, ensuring that your operations run smoother, safer, and more economically.
1. Uncompromising Safety: Your Top Priority, Our Core Principle
The inherent risks associated with the transportation, storage, and also handling of bulk sodium hypochlorite or chlorine gas are a significant concern for any safety-conscious organization. The SHOOT SHT-500G effectively eliminates these hazards.
On-Demand Generation: Our system produces sodium hypochlorite as needed, meaning you no longer have to store large quantities of hazardous chemicals on-site. This drastically reduces the risk of dangerous spills, leaks, and exposure to corrosive materials.
Low-Concentration Solution: The SHT-500G generates a sodium hypochlorite solution with a concentration of less than 1%. This solution is significantly less hazardous than commercial-grade chemicals, simplifying handling procedures and enhancing worker safety.
Elimination of Hazardous Transport: By generating your disinfectant on-site, you remove the need for frequent and also risky chemical deliveries, reducing traffic congestion at your facility and eliminating the potential for transportation-related accidents.
2. Significant Cost Reduction: A Smart Investment for a Healthier Bottom Line
The financial benefits of switching to SHT-500G are both immediate and long-term. This system is designed to provide a rapid return on investment by tackling operational costs from multiple angles.
Lower Chemical Expenditures: The primary raw materials for the SHT-500G are common salt and water, both of which are significantly more affordable than commercially produced sodium hypochlorite. This leads to substantial savings on your chemical procurement budget.
Reduced Transportation and Storage Costs: Eliminating the need for chemical deliveries and dedicated storage facilities frees up valuable capital and also operational resources.
Price Stability: You are no longer at the mercy of volatile chemical market prices. The cost of salt and electricity is far more stable, allowing for more predictable and manageable budgeting.
Optimized Dosing: The consistent purity and concentration of the on-site generated solution allow for precise and efficient dosing, preventing chemical wastage and further reducing consumption.
3. Unwavering Reliability and Consistency: The Cornerstone of Efficient Operations
Maintaining a consistent level of disinfectant is crucial for preventing biological growth, corrosion, and scaling in cooling water systems. The SHOOT SHT-500G delivers unparalleled reliability and consistency.
Fresh and Potent Solution: Commercially produced sodium hypochlorite degrades over time, losing its effectiveness. The SHT-500G, in contrast, produces a fresh solution on demand, ensuring maximum potency and optimal disinfection performance.
Precise Concentration Control: Our advanced system maintains a consistent output of sodium hypochlorite solution at the desired concentration, allowing for accurate and also automated dosing that adapts to the specific needs of your cooling water system.
Automated Operation: The SHT-500G is designed for fully automated, unattended operation. This minimizes the need for manual intervention, reduces the risk of human error, and also ensures continuous and reliable performance.
4. Environmental Responsibility: A Commitment to a Greener Future
In today’s environmentally conscious world, reducing your facility’s ecological footprint is more important than ever. The SHOOT SHT-500G is an environmentally responsible choice.
Reduced Carbon Footprint: By eliminating the transportation of bulk chemicals, you significantly reduce the carbon emissions associated with your water treatment program.
Elimination of Chemical Packaging Waste: The on-site generation process does away with the need for plastic drums and also containers, reducing plastic waste and its environmental impact.
Safer Discharge: The lower concentration of the generated sodium hypochlorite solution and the absence of degradation byproducts make for a more environmentally friendly discharge.
5. Simplicity of Operation and Maintenance: Designed for the Modern Industrial Plant
The SHOOT SHT-500G is engineered for user-friendliness and ease of maintenance, ensuring a seamless integration into your existing operations.
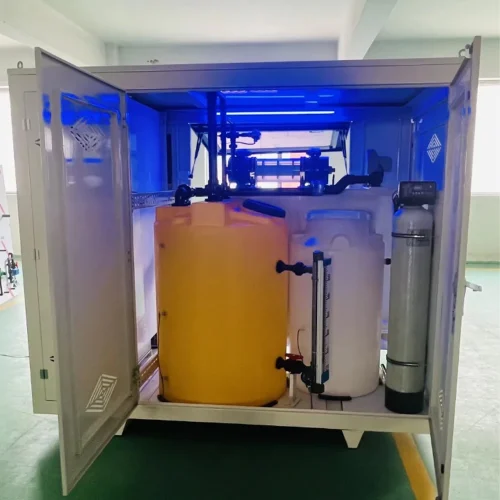
Intuitive Interface: The system features a user-friendly control panel that provides a clear overview of the operational status and also allows for easy adjustment of settings.
Durable and Robust Construction: Built with high-quality, corrosion-resistant materials, the SHT-500G is designed to withstand the rigors of an industrial environment, ensuring a long and reliable service life.
Modular Design: The modular construction of the system simplifies maintenance and allows for easy access to all components, minimizing downtime and service costs.

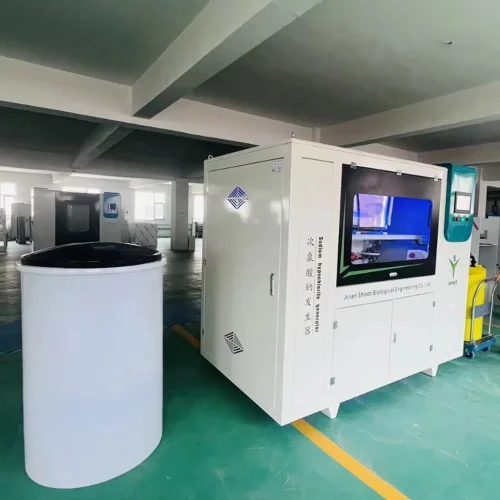
2. Sodium hypochlorite generator parameter
| Product name | SHT-500G |
|---|---|
| Effective chlorine yield | 500g/H |
| Concentration | 6-8g/L(6000-8000ppm) |
| Power | 3KW |
| Salt consumption | 3.2KG/KG |
| Size | 2600*900*2000mm |
| Voltage | 380V/50hz |
3. The SHOOT Service Advantage: Your Partner in Excellence
At SHOOT, we believe that providing a superior product is only half of the equation. We are committed to delivering an exceptional service experience that ensures you get the most out of your investment in the SHT-500G Sodium Hypochlorite Generator at the same time. Our comprehensive service and support program is designed to be your trusted partner every step of the way.
1. Expert Consultation and System Design
Our team of experienced water treatment specialists will work closely with you to understand the unique requirements of your cooling water system. We will conduct a thorough assessment of your facility and recommend a customized solution that is perfectly tailore to your needs.
2. Seamless Installation and Commissioning
Our certified technicians will ensure a smooth and also efficient installation process, minimizing disruption to your operations. We take a meticulous approach to every installation, ensuring that your new system is integrate seamlessly into your existing infrastructure.
3. Comprehensive Operator Training
We empower your team with the knowledge and skills they need to operate and maintain the SHOOT SHT-500G with confidence. Our training programs are design to be practical and hands-on, covering all aspects of the system’s operation. This includes:
Detailed instruction on system functionality and control.
Best practices for routine maintenance and also troubleshooting.
Safety procedures and protocols.
Ongoing access to our technical support team for any questions.
4. Responsive and Reliable Technical Support
We understand that uptime is critical to your success. That is why we offer responsive and reliable technical support to address any issues that may arise. Our dedicated support team is available to provide:
24/7 remote monitoring and diagnostics.
Prompt on-site assistance from our qualified technicians.
A comprehensive inventory of spare parts for quick and efficient repairs.
A commitment to resolving your issues as quickly as possible.
5. Customized Preventive Maintenance Programs
To ensure the long-term reliability and performance of your SHOOT SHT-500G, we offer customized preventive maintenance programs. These programs are designed to proactively identify and address potential issues before they become major problems.
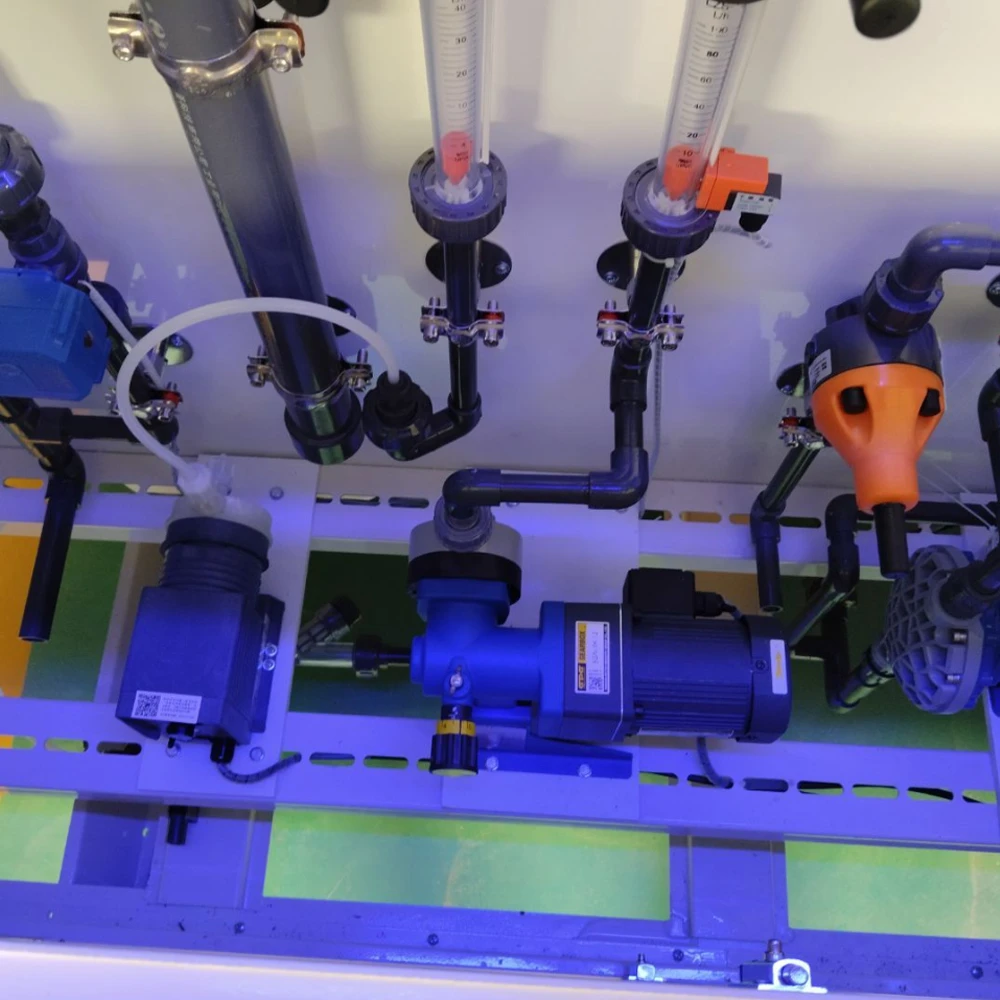
4. Applications of SHT-500G in Large-Scale Water Treatment
The robust capacity and advanced features of SHT-500G make it the ideal disinfection solution for a wide range of large-scale water treatment applications. Its versatility and reliability are unmatched in the industry.
1. Municipal Drinking Water Treatment Plants
The primary application for the SHT-500G is in large municipal drinking water treatment plants. With a production capacity of 500 grams of chlorine equivalent per hour, it can effectively disinfect vast quantities of water, ensuring that it is safe for public consumption. Its automated operation and remote monitoring capabilities make it a perfect fit for the complex and demanding environment of a modern waterworks.
2. Wastewater Treatment Facilities
Effective disinfection is also a critical final step in the wastewater treatment process to protect receiving water bodies. SHT-500G can be seamlessly integrate into wastewater treatment plants to ensure that the treated effluent meets all regulatory standards before being discharge into the environment. Its reliable and cost-effective operation makes it an attractive alternative to traditional disinfection methods in this sector.
3. Industrial Water Treatment
Many industrial processes require large volumes of high-quality, disinfected water. The SHT-500G can be utilized in a variety of industrial settings, including power plants, manufacturing facilities, and food and beverage processing plants, to ensure that the water used in their processes is free from harmful microorganisms. Its on-site generation capabilities provide a consistent and reliable supply of disinfectant, crucial for maintaining operational efficiency and product quality.
4. Cooling Tower Water Treatment
The growth of microorganisms in cooling towers can lead to biofouling, corrosion, and the proliferation of harmful bacteria such as Legionella. SHT-500G provides an effective and automated solution for treating cooling tower water, preventing these issues and ensuring the safe and efficient operation of cooling systems.

5. A Trusted Partner in Over 30 Countries

FAQ
1. Is on-site generation safer than liquid chlorine?
Yes! No toxic gas storage or transport risks. The system produces only what you need at the same time.
2. What’s the maintenance requirement?
Minimal. Regular cell cleaning and also salt refills. Automated alerts simplify upkeep.
3. How to handle maintenance?
Automated alerts guide servicing.
Factory advantage
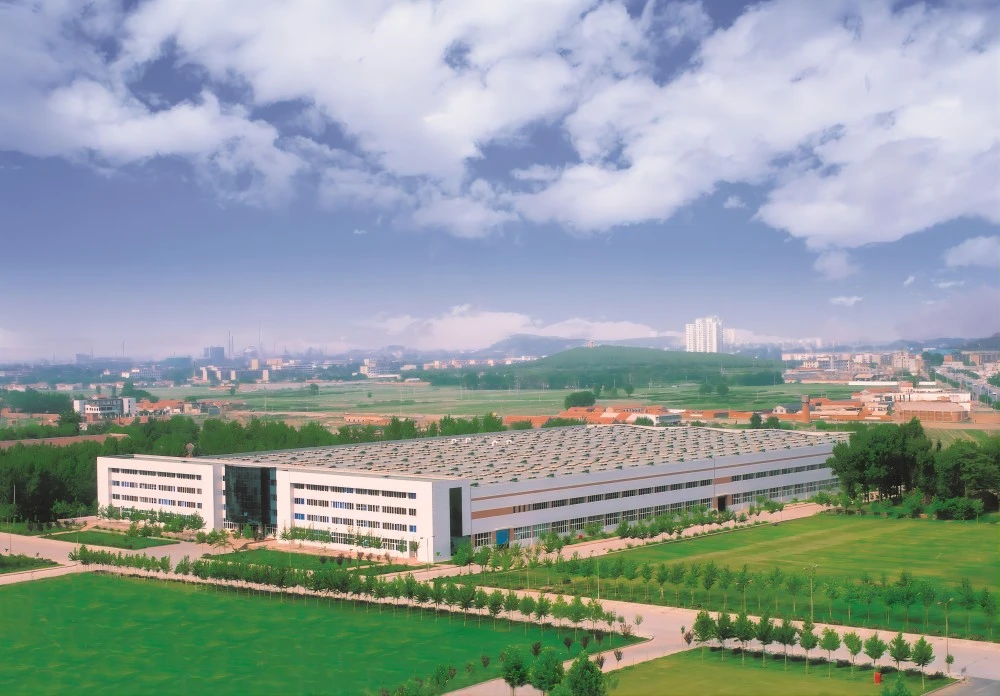
We have R&D centers, production centers, data centers and marketing centers. It is committe to providing technical support and innovative applications for improving public health security. Since its establishment, the company has obtained 12 invention patents and environmental management system certification. The company also has more than 30 test reports, covering surface and other different concentration detection projects. The series products sell well all over the country, and exported to such as Thailand, Malaysia, Cambodia, Brazil, South Africa, South America and other more than 20 countries and regions. The company has a perfect product sales and service system. To meet the needs of different customers with more professional services. So that to provide the best products and services for public health!
Customer feedback