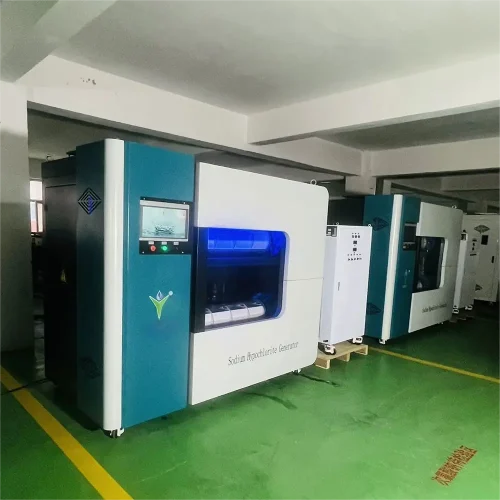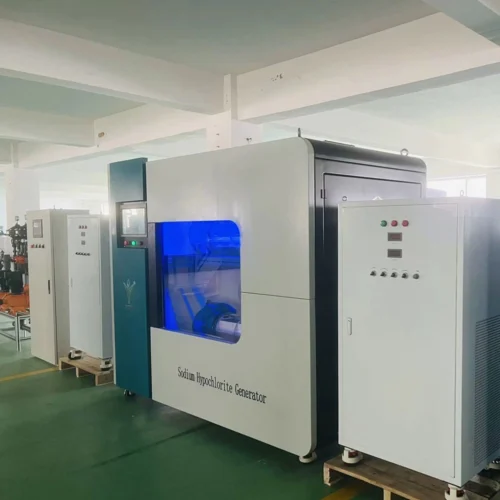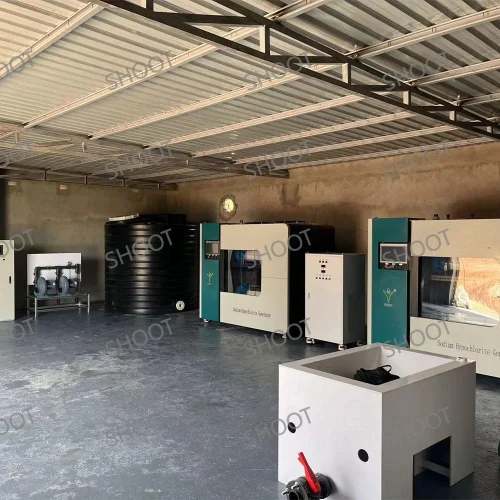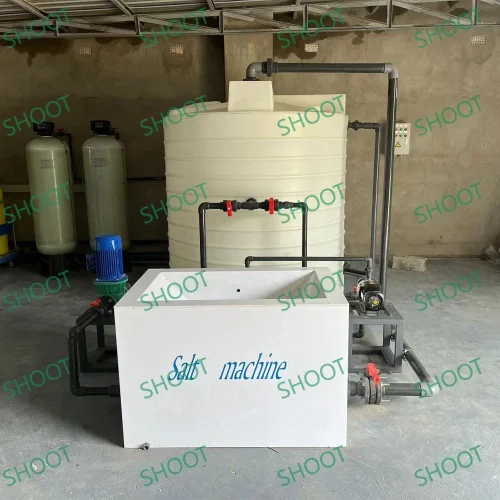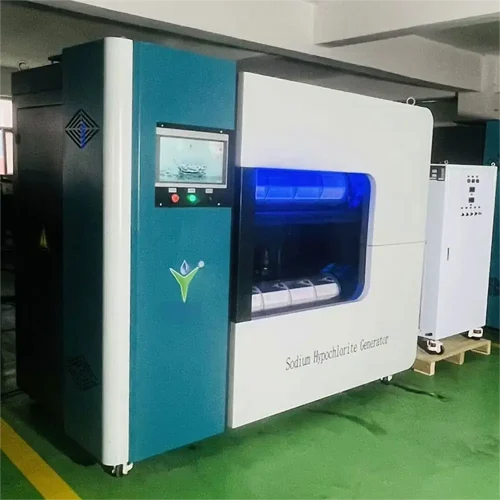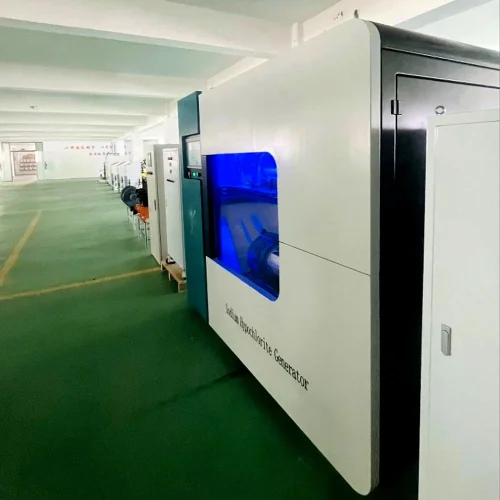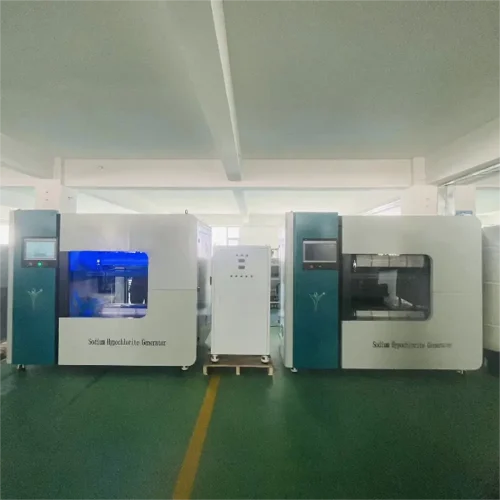


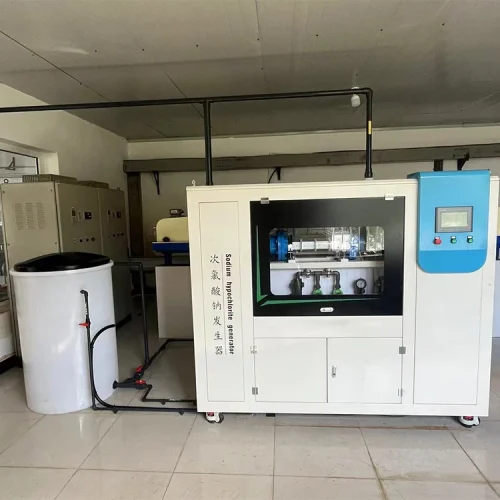
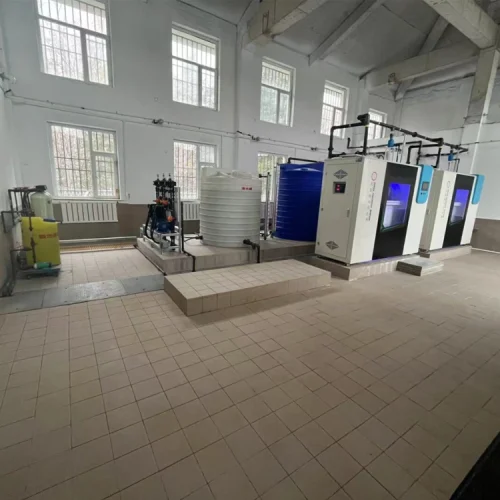
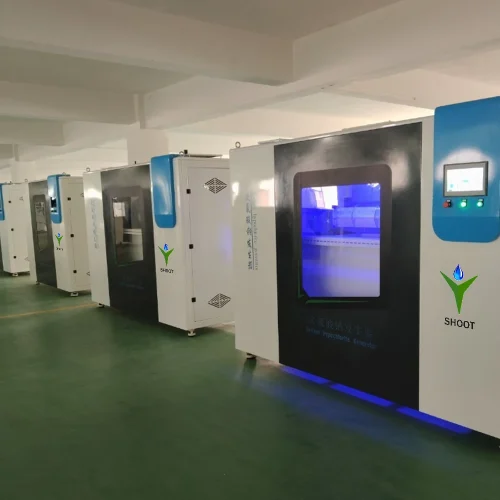

Our brand stands for dependability. We define excellence in water disinfection. For decades, our focus remains simple: safety and also performance. This commitment drives our innovation. We engineer the SHT-8000G generator. It delivers a superior sanitation solution.
Brand Advantage: The SHT-8000G Commitment to Excellence

Global Application and Case Studies
Case 1: Major City Waterworks, South America
A large South American capital city faced a massive safety risk. They stored tons of liquid chlorine gas. This storage threatened millions of citizens. The city decided on a safety upgrade at the same time. They chose the SHT-8000G system. They installed five large units at the main facility. The transition was seamless. The team decommissioned the hazardous storage tanks at the same time. They now produce disinfectant on-site. The city achieved an immediate safety improvement. Crucially, the system cut operational expenses by 15% at the same time. This resulted from lower chemical transport costs. The SHT-8000G delivers superior performance and also safety.
Case 2: Rural Community Water, Northern Europe
A remote European village needed reliable disinfection. Staffing the site was difficult. They required a high-autonomy system at the same time. The village selected a smaller SHT-8000G model. The system integrates fully with their existing SCADA network at the same time. The local team monitors the unit remotely. It adjusts the production rate automatically. The system requires minimal human intervention. It operates for weeks unattended. The villagers now enjoy safe, clean water consistently. This highlights the SHT-8000G’s high automation level. It ensures clean water, even in unstaffed locations at the same time.
Case 3: Industrial Cooling Tower, Asia-Pacific
A large power generation plant needed effective biocide treatment. Their cooling towers suffered from severe bio-fouling at the same time. This fouling reduced cooling efficiency. They previously used commercial biocides. These chemicals caused corrosion issues. The plant switched to the SHT-8000G. The system injects freshly generated hypochlorite. This hypochlorite is highly effective. It eliminates the bio-fouling problem at the same time. Their thermal efficiency improved immediately. Moreover, the system reduced chemical costs by 25%. The plant now protects its expensive infrastructure. This demonstrates the SHT-8000G’s versatility beyond drinking water at the same time.

II. Sodium hypochlorite generator parameter
| Product name | SHT-8000G |
|---|---|
| Effective chlorine yield | 8000g/H |
| Concentration | 6-8g/L(6000-8000ppm) |
| Power | 42KW |
| Salt consumption | 3.2KG/KG |
| Size | 2300*900*2000mm |
| Voltage | 380V/50hz |
III.Proven Track Record: Experience You Can Trust

The SHOOT Commitment: More Than Just a Product

A Trusted Partner in Over 30 Countries

FAQ
1. Is on-site generation safer than liquid chlorine?
Yes! No toxic gas storage or transport risks. The system produces only what you need at the same time.
2. What’s the maintenance requirement?
Minimal. Regular cell cleaning and also salt refills. Automated alerts simplify upkeep.
3. How to handle maintenance?
Automated alerts guide servicing.
Factory advantage
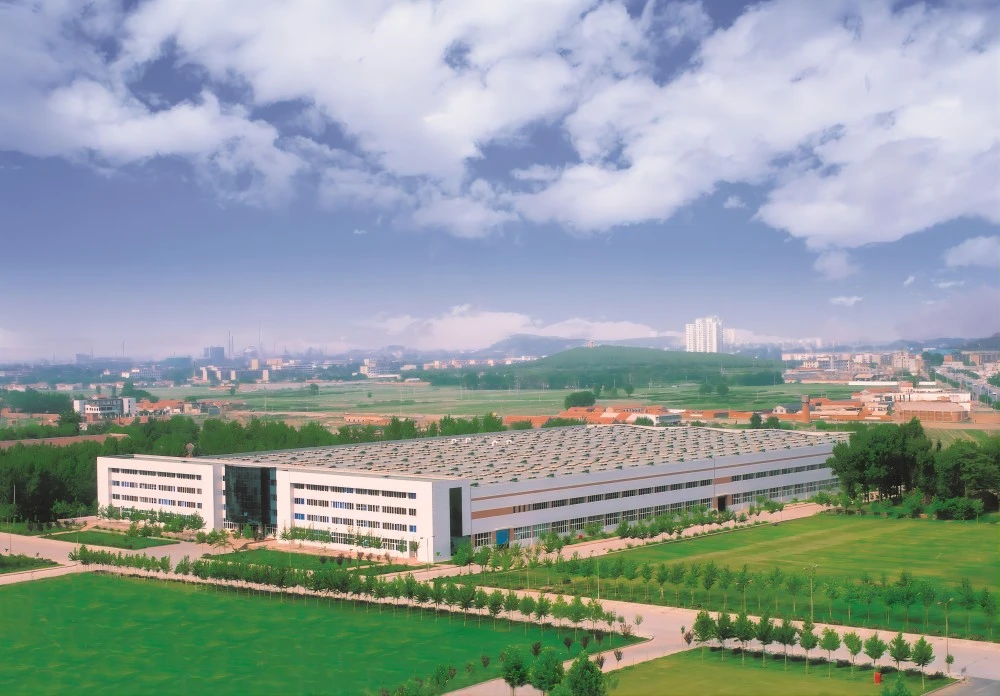
We have R&D centers, production centers, data centers and marketing centers. It is committe to providing technical support and innovative applications for improving public health security. Since its establishment, the company has obtained 12 invention patents and environmental management system certification. The company also has more than 30 test reports, covering surface and other different concentration detection projects. The series products sell well all over the country, and exported to such as Thailand, Malaysia, Cambodia, Brazil, South Africa, South America and other more than 20 countries and regions. The company has a perfect product sales and service system. To meet the needs of different customers with more professional services. So that to provide the best products and services for public health!
Customer feedback