



ndMunicipal water treatment faces constant challenges. You need reliable, safe, and efficient disinfection. Moreover, you must meet strict regulatory standards. You also need to control costs and simplify operations. Traditional chlorine gas poses safety risks. Transporting and storing bulk sodium hypochlorite (bleach) is costly and also leads to degradation.
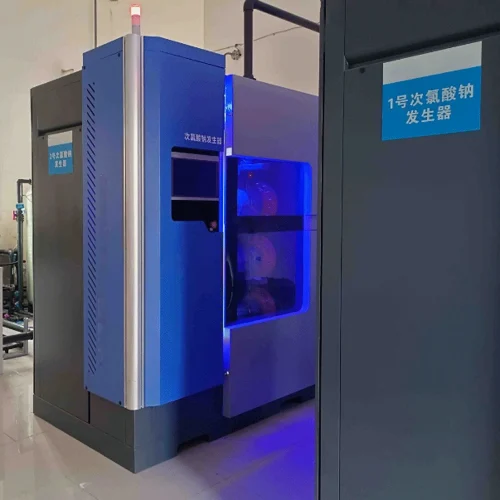
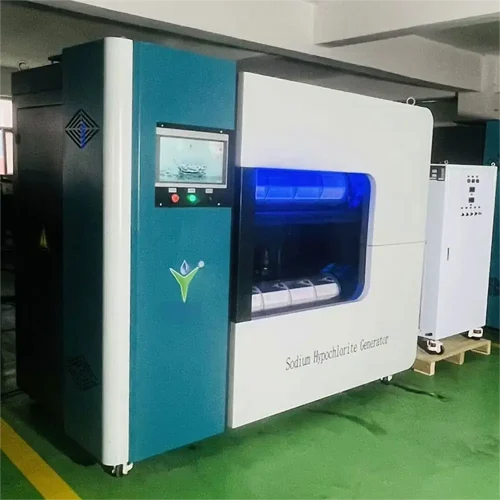
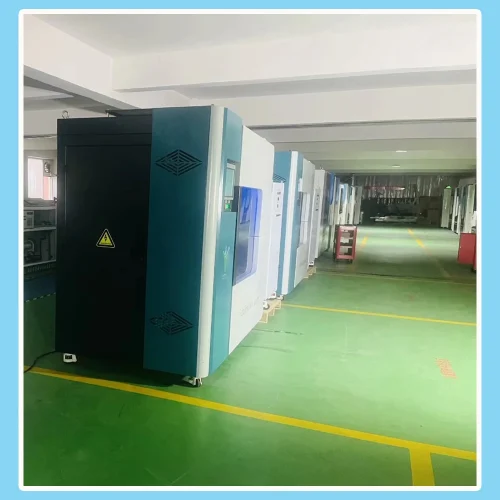
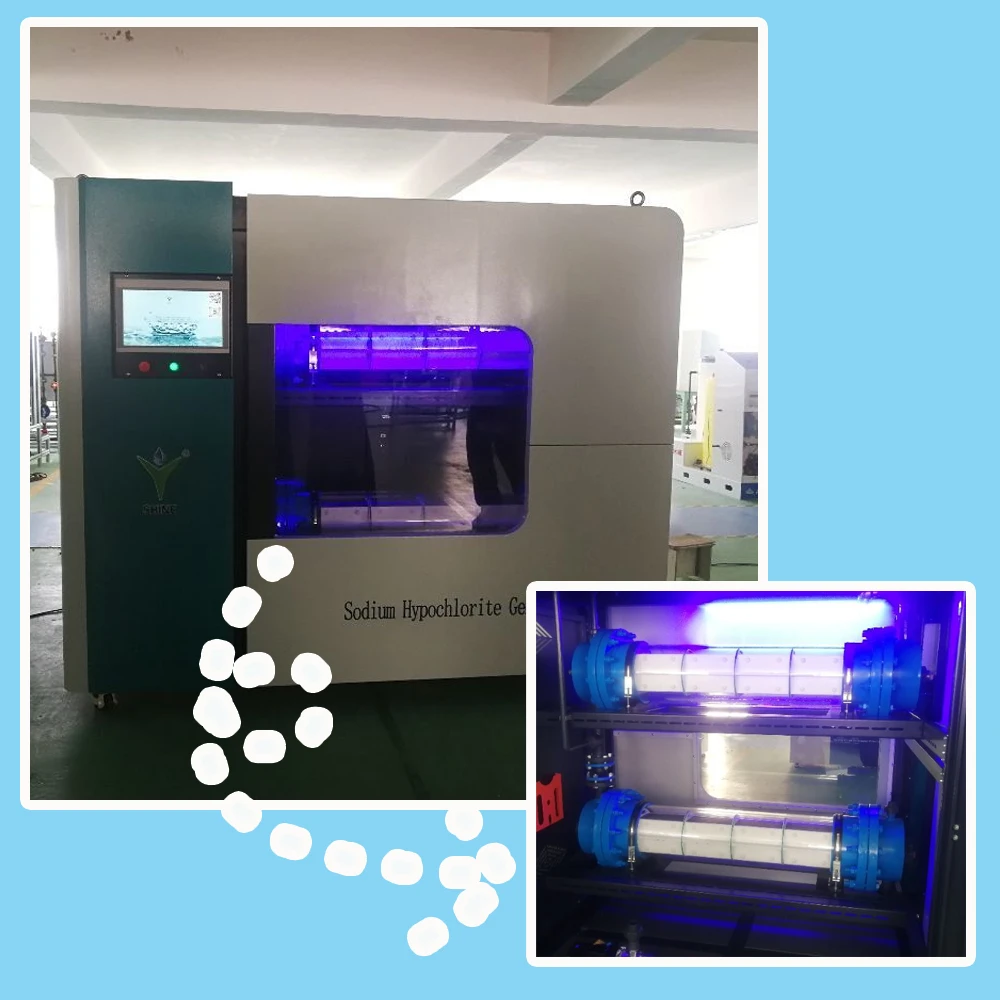
There is a better way. Meet the SHT-10000G Sodium Hypochlorite Generator. This system produces a powerful disinfectant on-site, right when you need it. We designed it specifically for large-scale municipal water plants. Our focus is on integration, intelligence, and also robust performance.
The SHT-10000G is not just a generator. It is a complete disinfection solution. It transforms common salt, water, and also electricity into a consistent supply of high-quality sodium hypochlorite. This eliminates hazardous chemical handling. It also ensures your disinfectant is always fresh and potent.
Core Advantage 1: Unmatched System Integration
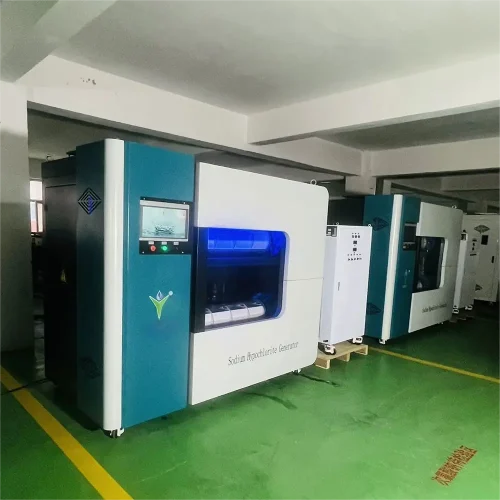
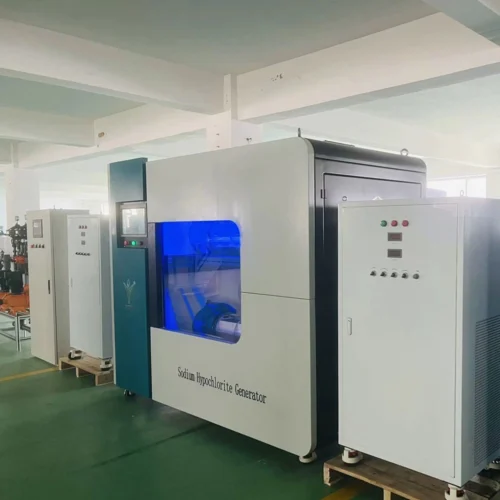
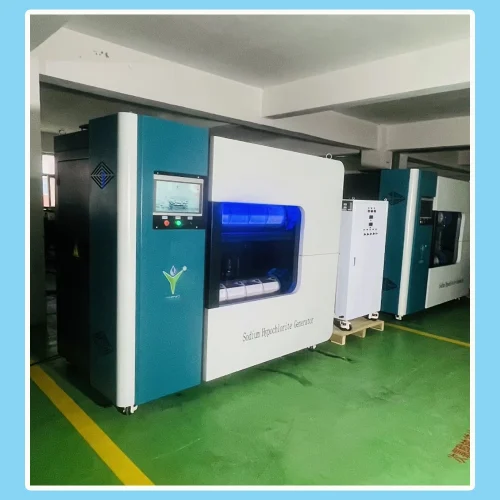
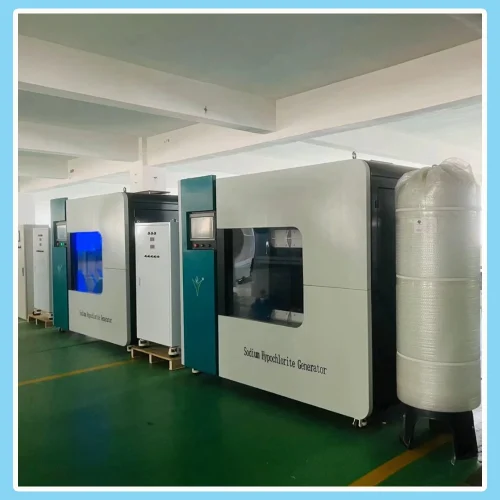
SHT-10000G stands out because of its total integration. We deliver a fully assembled, pre-tested skid. This approach offers significant benefits from day one.
1. Plug-and-Play Installation.
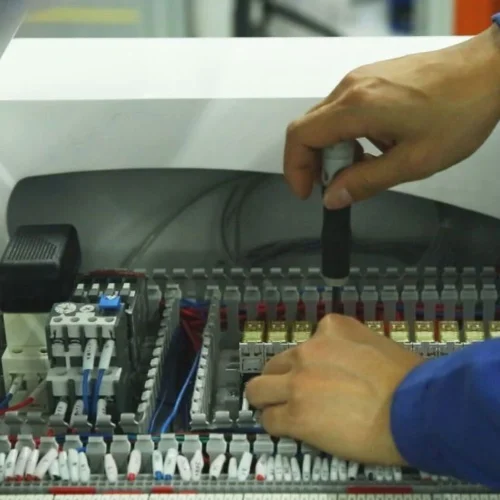
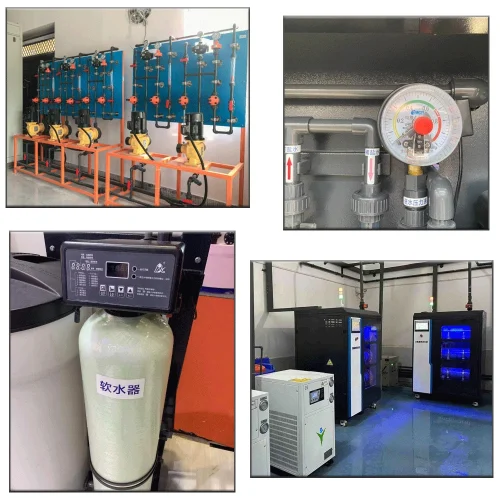
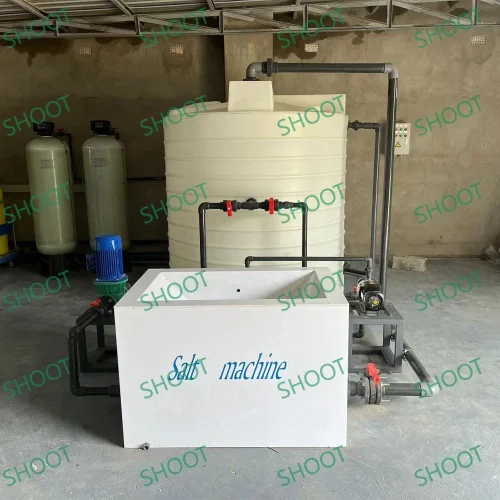
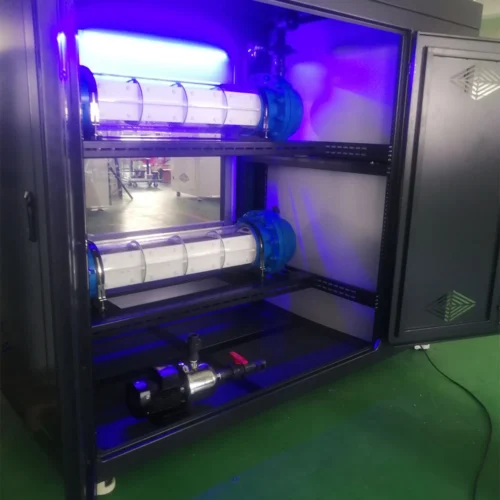
Forget complex, multi-vendor setups. Our unit arrives ready for connection. The skid includes all major components. You get the electrolytic cell, rectifier, salt dissolver, softening system, and also dosing pumps. Everything is pre-mounted and pre-wired on a single, robust frame. This drastically reduces installation time and also costs. Your team simply connects utilities and aslo piping.
2. Optimized Internal Design.
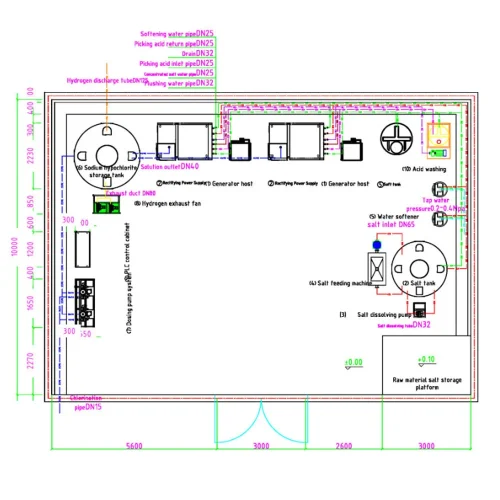
Our engineers designed the system for perfect component synergy. Flow paths are short and also efficient. This minimizes pressure drops, and aslo energy use. The layout also allows for easy, safe access for maintenance. Every part works in harmony for peak performance.
3. Space-Saving Footprint.
Large plants often have limited space. The SHT-10000G’s compact, integrated design solves this problem. It requires a much smaller footprint than assembling individual components. This efficient use of space is a major advantage for plant upgrades and also expansions.
4. Simplified Training and Operation.
Operators interact with one unified system, not a collection of disparate parts. This simplifies training significantly. Staff quickly learn the straightforward control logic. They can manage the entire disinfection process from a single point.

2. Sodium hypochlorite generator parameter
| Product name | SHT-10000G |
|---|---|
| Effective chlorine yield | 10000g/H |
| Concentration | 6-8g/L(6000-8000ppm) |
| Power | 60KW |
| Salt consumption | 3.2KG/KG |
| Size | 2600*900*2000 |
| Voltage | 380V/50hz |
Core Advantage 2: Advanced Network Connectivity and Smart Control
SHT-10000G is a smart device built for the digital age. It turns disinfection from a manual task into an automated, data-driven process at the same time.
1. Remote Monitoring and Control.
The system features a standard Ethernet port. Connect it directly to your plant’s network. This allows real-time monitoring from any authorized workstation at the same time. Operators can view key parameters remotely. They see production rates, solution strength, salt levels, and also system status instantly. They can also adjust setpoints or start/stop production without being physically present at the skid.
2. Seamless Integration.
The generator communicates using standard industrial protocols like Modbus TCP/IP. Integration into your existing control architecture is smooth and also reliable. This provides a holistic view of your plant’s operations. Disinfection data becomes part of your overall process management.
3. Proactive Data Logging and Alarms.
The built-in PLC continuously records operational data. It tracks performance trends over time. More importantly, the system generates immediate alerts for any irregular condition at the same time. It warns of low salt, low flow, or power fluctuations. This enables proactive maintenance. Your team can address small issues before they become big problems, maximizing uptime.
4. Enhanced Regulatory Compliance.
Automated data logging creates accurate, verifiable records. You can easily generate reports for regulatory bodies. The system provides proof of consistent disinfectant production and also dosage. This simplifies compliance and auditing processes.
Core Advantage 3: Superior Environmental Adaptability
Water plants operate in diverse climates and conditions. SHT-10000G is built to perform reliably, everywhere.
1. Tolerance to Water Quality Variations.
Source water quality can change. Our system includes an integral, high-efficiency water softener. This protects the sensitive electrolytic cell from scaling caused by water hardness. It ensures optimal efficiency and also a long cell life, even with varying feedwater quality.
2. Wide Operating Temperature Range.
The system functions effectively across a broad ambient temperature range. Key components are housed in a protected, environmentally controlled cabinet at the same time. This safeguards them from extreme heat or cold. Whether in a hot desert climate or a cold northern region, performance remains stable.
3. Built for Demanding Environments.
We construct the skid with industrial-grade materials. Critical wetted parts use corrosion-resistant polymers and also titanium. This ensures long-term durability in humid or mildly corrosive environments typical of water treatment plants at the same time. The system is rugged and also dependable.
4. Reduced Temperature Dependency of Output.
Unlike stored bleach, which loses strength in heat, the SHT-10000G produces a consistent concentration on demand. You are not affected by the thermal degradation that weakens delivered liquid bleach during storage.

5. A Trusted Partner in Over 30 Countries
Key Technical Specifications (SHT-10000G Model):
Production Capacity: Up to 10,000 grams of available chlorine per hour at the same time.
Solution Concentration: Approximately 0.8% (8,000 ppm).
Primary Raw Materials: Salt (NaCl), Water, Electricity.
Salt Consumption: Approximately 3.0 – 4.0 kg per kg of available chlorine at the same time.
Power Consumption: Approximately 3.5 – 4.5 kWh per kg of available chlorine at the same time.
Control System: Integrated PLC with color touchscreen HMI.
Connectivity: Standard Ethernet port with Modbus TCP/IP protocol.
Conclusion: The Future of Municipal Disinfection is On-Site, Integrated, and also Smart

FAQ
1. Is on-site generation safer than liquid chlorine?
Yes! No toxic gas storage or transport risks. The system produces only what you need at the same time.
2. What’s the maintenance requirement?
Minimal. Regular cell cleaning and also salt refills. Automated alerts simplify upkeep.
3. How to handle maintenance?
Automated alerts guide servicing.
Factory advantage
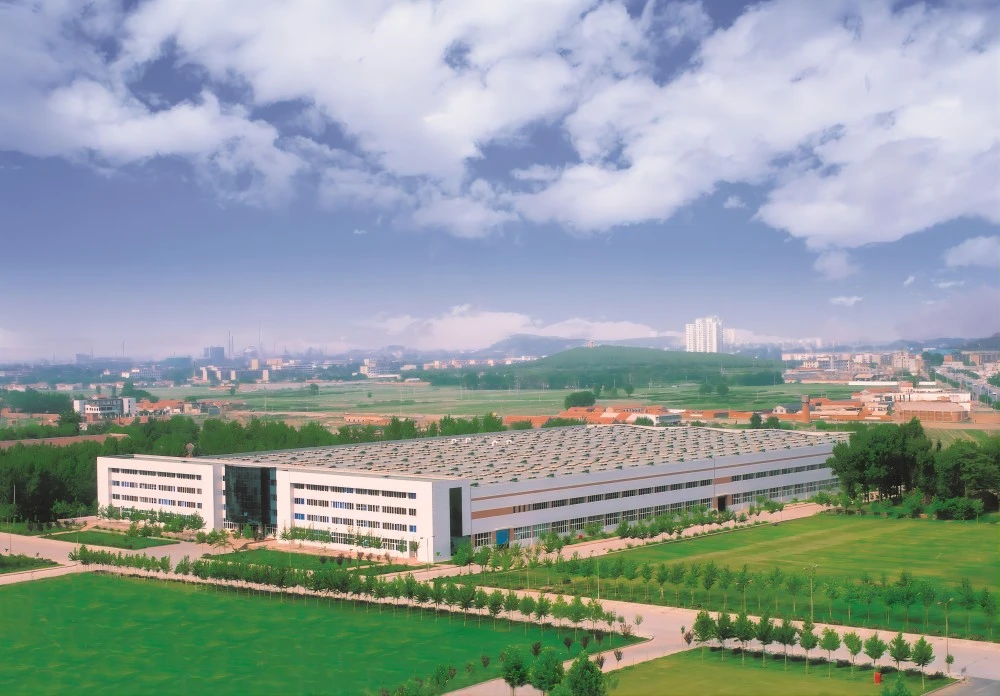
We have R&D centers, production centers, data centers and marketing centers. It is committe to providing technical support and innovative applications for improving public health security. Since its establishment, the company has obtained 12 invention patents and environmental management system certification. The company also has more than 30 test reports, covering surface and other different concentration detection projects. The series products sell well all over the country, and exported to such as Thailand, Malaysia, Cambodia, Brazil, South Africa, South America and other more than 20 countries and regions. The company has a perfect product sales and service system. To meet the needs of different customers with more professional services. So that to provide the best products and services for public health!
Customer feedback