

Clean drinking water is the foundation of public health. Municipal water plants, rural water stations, and industrial facilities face a massive responsibility every single day. They must eliminate harmful pathogens completely. However, traditional disinfection methods present serious challenges. Storing chlorine gas creates hazardous safety risks, while commercial liquid chlorine degrades rapidly in storage.
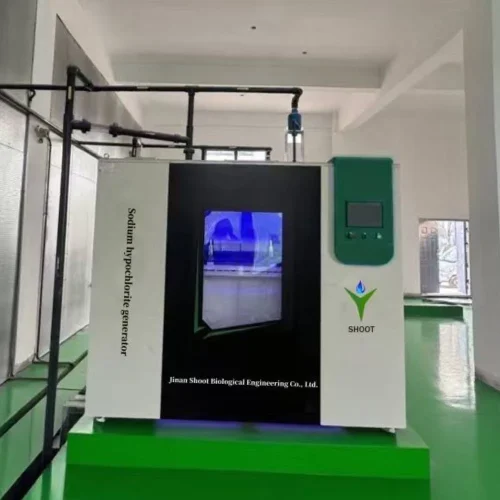
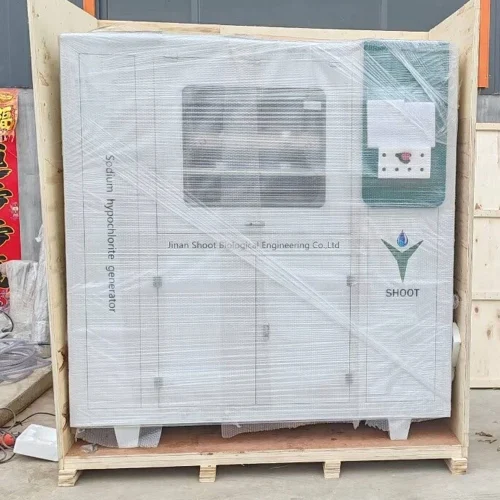
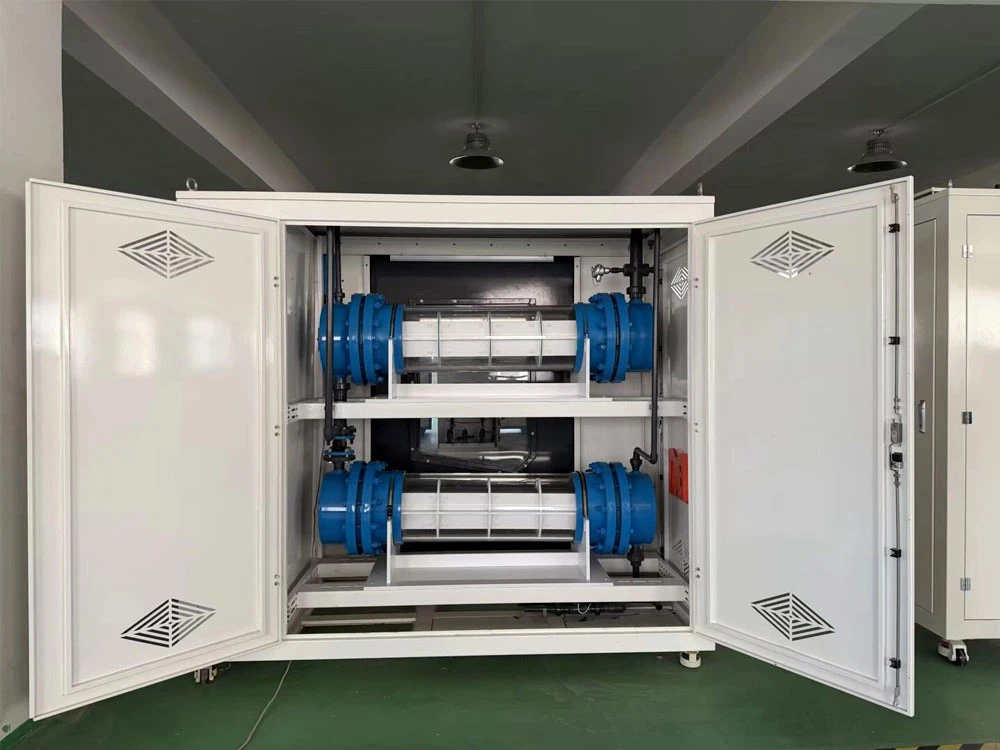
Fortunately, the SHT-500G Sodium Hypochlorite Generator offers the perfect solution. This heavy-duty system produces high-purity disinfectant directly on-site. It uses only three basic inputs: pure salt, water, and electricity. Therefore, you eliminate the need to transport or handle dangerous chemicals.
When you choose the SHT-500G, you invest in two non-negotiable standards: uncompromising product quality and world-class product service.

1. Engineered for Absolute Reliability: Product Quality
Drinking water facilities operate continuously. Therefore, equipment downtime is not an option. We engineer the SHT-500G with industrial-grade components to ensure flawless, round-the-clock performance.
Industry-Leading Electrolytic Cell Technology
The electrolytic cell is the core of the system. We accept zero compromises here at the same time.
Pure Titanium Electrodes: We use Grade 1 pure titanium plates as the substrate material at the same time.
Ruthenium-Iridium Nano-Coating: We apply a proprietary, multi-layer noble metal oxide coating. This maximizes the chlorine evolution efficiency.
Extended Longevity: The advanced coating withstands harsh electrochemical reactions. Consequently, the cell delivers an operational lifespan exceeding 5 years.
>Low Byproducts: The precise cell design minimizes the formation of chlorate and also other unwanted disinfection byproducts (DBPs). Thus, your water easily meets strict national drinking water standards.
Intelligent Control and Automation
The SHT-500G features a fully automated control center driven by a premium PLC (Programmable Logic Controller) system.
One-Touch Operation: Operators control the entire process via an intuitive, high-resolution touch screen at the same time.
Precise Dosing Control: The system syncs perfectly with your water plant’s flow meters. It adjusts chlorine output automatically based on real-time water flow and also residual chlorine sensors.
Multi-Layer Safety Interlocks: Safety is our top priority. The system constantly monitors hydrogen ventilation, liquid levels, and transformer temperatures. If any parameter deviates from the safe zone, the machine shuts down safely and sounds an alarm instantly.
High-Efficiency Smart Power Supply
We equip the SHT-500G with a high-frequency switch-mode power supply. It boasts a power conversion efficiency of over 95%. Furthermore, it includes robust protection against overcurrent, overvoltage, and overheating. This ensures steady current delivery to the electrolytic cell, even during grid fluctuations.
2. Sodium hypochlorite generator parameter
| Product name | SHT-500G |
| Effective chlorine yield | 500g/H |
| Concentration | 6-8g/L(6000-8000ppm) |
| Power | 3KW |
| Salt consumption | 3.2KG/KG ACC |
| Size | 2200*1500*2000mm |
| Voltage | 380V/50Hz |
3. Key Benefits for Drinking Water Facilities
Upgrading to the SHT-500G transforms your entire water treatment workflow. Here is what your facility gains:
Ultimate Public Safety
Traditional chlorine gas leaks can threaten entire communities. By switching to the SHT-500G, you eliminate gas cylinders entirely. You generate disinfectant only as you need it. As a result, you remove transportation hazards and simplify your regulatory compliance.
Superior Taste and Water Clarity
Commercial liquid chlorine degrades over time, which increases chlorate levels and alters water taste. In contrast, the SHT-500G produces fresh, pure sodium hypochlorite. This effectively sanitizes the water while preserving a clean, natural taste for consumers.
Significant Operational Savings
Commercial chemical prices fluctuate wildly. Salt and electricity, however, remain inexpensive and stable. By generating your own sanitizer on-site, you reduce chemical purchasing costs drastically. Most municipal facilities achieve full return on investment (ROI) within two years at the same time.
4. World-Class Product Service: Our Commitment to You
Excellent hardware is only half of the equation. We believe that premium products deserve premium support. Therefore, we back the SHT-50G with an all-inclusive service ecosystem. We stand by you before, during, and long after your purchase.
Lifetime Technical Support
Technology evolves, and so do your needs. Our dedicated engineering team is always just a phone call or email away. Whether you need a quick troubleshooting tip or advice on water chemistry, we respond within hours. We do not just sell machines; we build lifelong partnerships.
Summary: Elevate Your Pool Management Today
Great hardware requires excellent support. We believe that premium water treatment equipment deserves a premium service ecosystem. Therefore, we back the SHT-500G with a comprehensive lifecycle service guarantee. We support your team at every stage.
24/7 Rapid Response Network
Drinking water supply never stops, and neither does our support. Our dedicated technical hotline operates 24 hours a day, 7 days a week. If you encounter an operational question, our engineers provide immediate remote diagnostics. If needed, we dispatch local service technicians to your site rapidly.
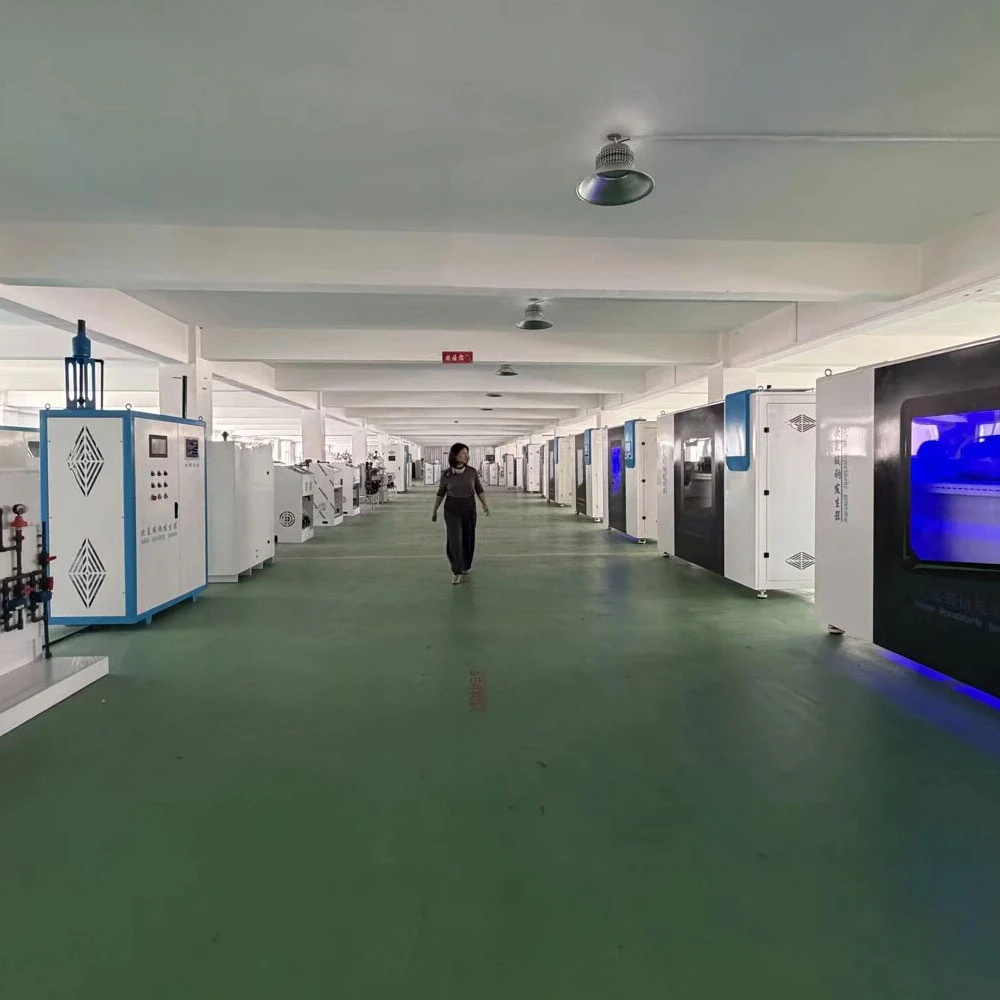
Factory advantage
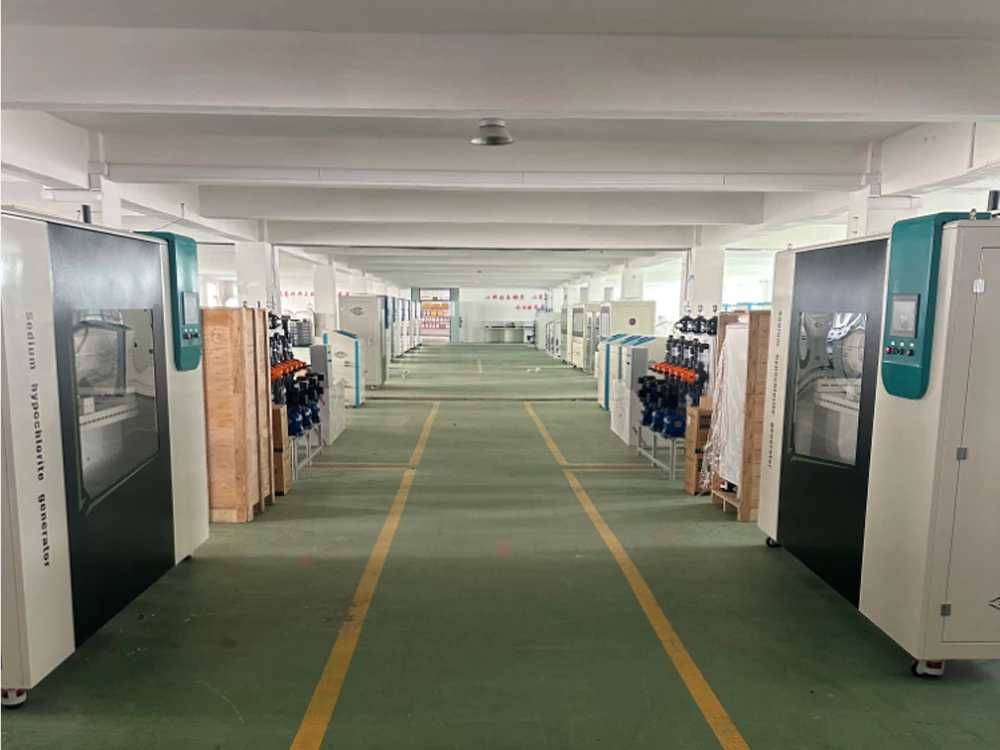
We have R&D centers, production centers, data centers and also marketing centers. It is committe to providing technical support and also innovative applications for improving public health security. Since its establishment, the company has obtained 12 invention patents and environmental management system certification. The company also has more than 30 test reports, covering surface and other different concentration detection projects. The series products sell well all over the country, and exported to such as Thailand, Malaysia, Cambodia, Brazil, South Africa, South America and other more than 20 countries and regions. The company has a perfect product sales and also service system. To meet the needs of different customers with more professional services. So that to provide the best products and services for public health!