


Access to safe, clean drinking water is fundamental. For rural communities, achieving this can be a significant challenge. Traditional water disinfection methods often involve handling hazardous chemicals, high operational costs, and also complex logistics. This is outdated. There is a better way.
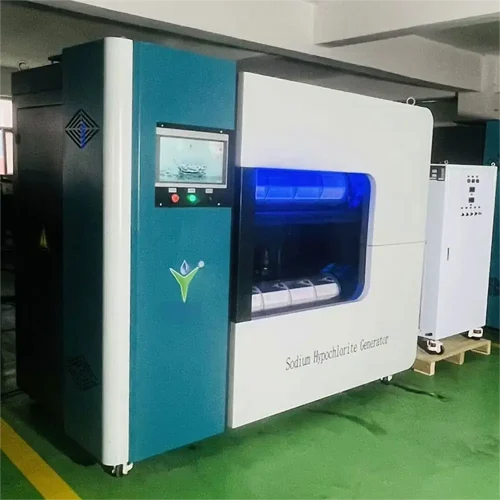
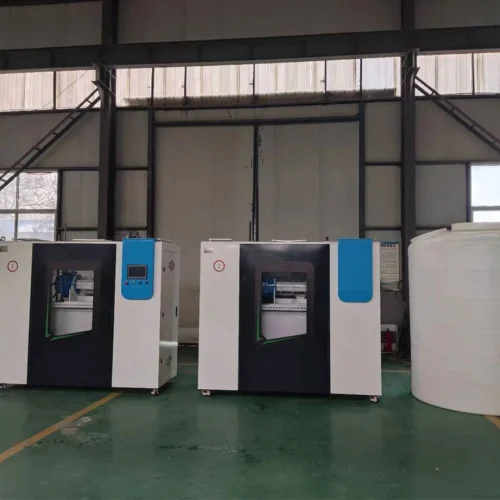
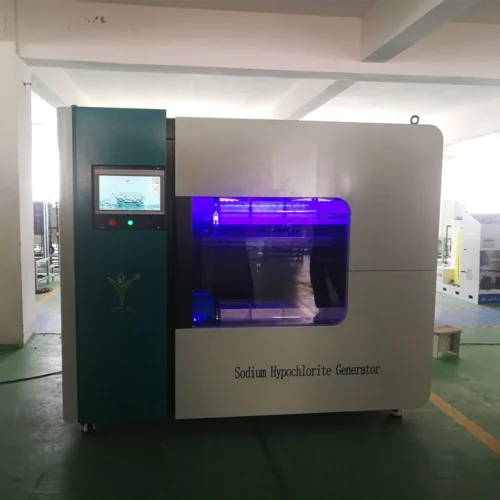
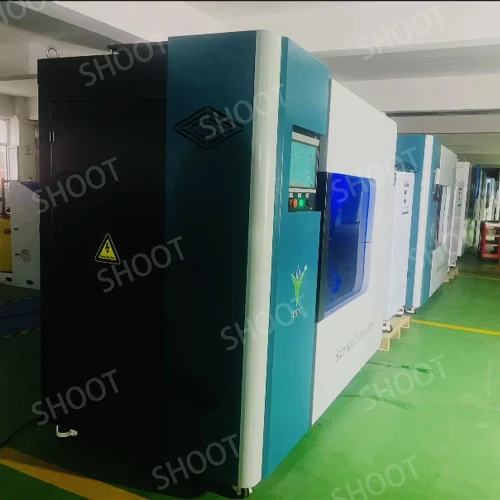
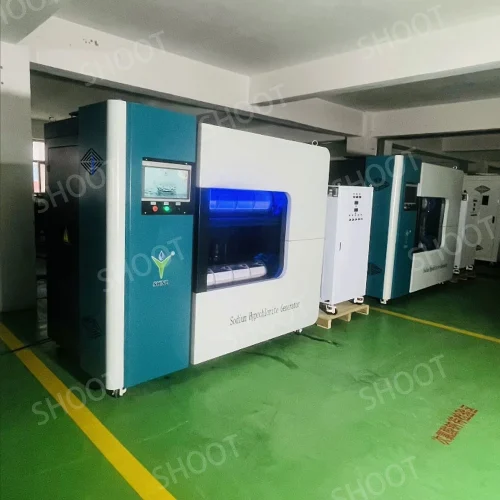
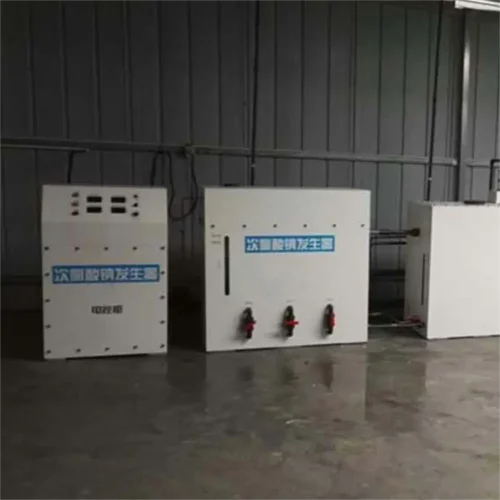
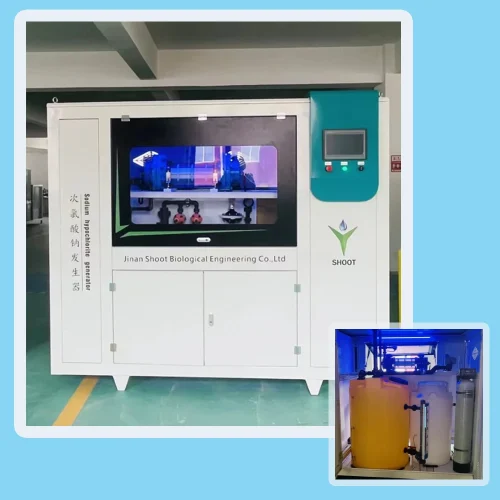
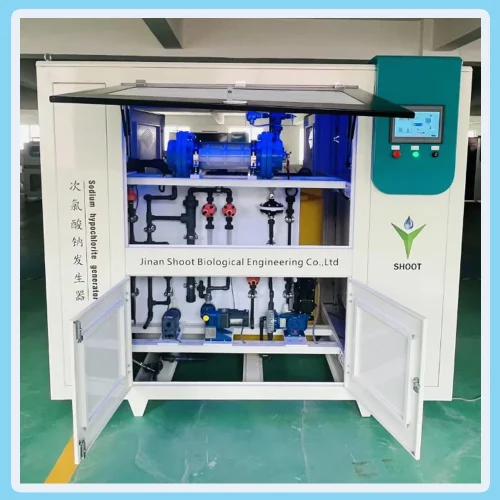
We introduce SHT-50G On-Site Sodium Hypochlorite Generator. This innovative system empowers rural communities and also water treatment plants. It produces a powerful disinfectant right where you need it. No more dangerous chemical transport. No more complex storage requirements. Just consistent, reliable, and also safe water disinfection.
1. The Core Advantage of On-Site Generation
First, understand the “why.” Why choose on-site generation over traditional methods?
1. Total Elimination of Chemical Handling.
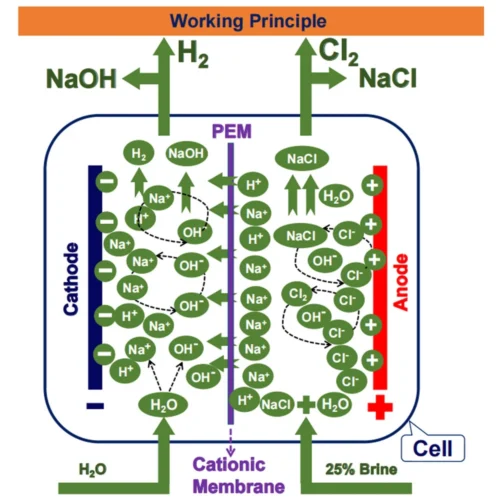
Traditional chlorine gas is highly toxic. Liquid sodium hypochlorite (bleach) degrades quickly. Both require frequent transportation and careful storage. Our system removes these risks entirely. You only need three simple, safe ingredients: salt, water, and also electricity.
2. Unmatched Disinfection Performance.
Sodium hypochlorite is a proven, powerful disinfectant. It effectively eliminates bacteria, viruses, and also other pathogens. It protects water throughout the distribution system. Best of all, you produce it on-demand. This means you always use a fresh, highly potent solution. Therefore, you never deal with the weak, degraded bleach that arrives after long-distance shipping.
3. Simple and Stable Raw Materials.
Salt is safe, stable, and inexpensive. It is easy to source and store in large quantities. You convert this simple material into your primary disinfectant. This process provides incredible operational security and also peace of mind.

2. Sodium hypochlorite generator parameter
| Product name | SHT-50G |
|---|---|
| Effective chlorine yield | 50g/H |
| Concentration | 6-8g/L(6000-8000ppm) |
| Power | 1.5KW |
| Salt consumption | 3.2KG/KG |
| Size | 2600*900*2000mm |
| Voltage | 380V/50hz |
3. The Power of (High Integration) and IoT Connectivity
Our SHT-50G system is not just a generator. It is a fully integrated water treatment solution. We designed it for simplicity, reliability, and also modern control.
1. A Complete, Plug-and-Play Solution.
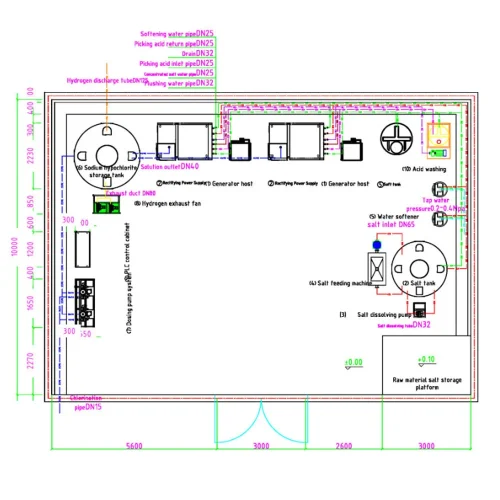
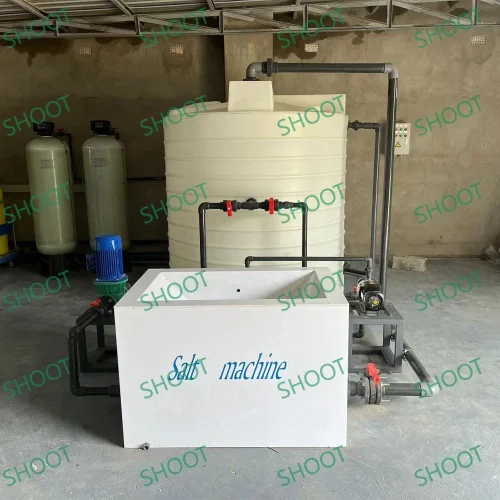
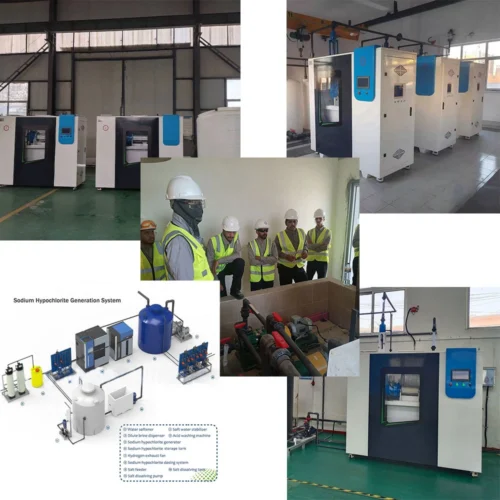
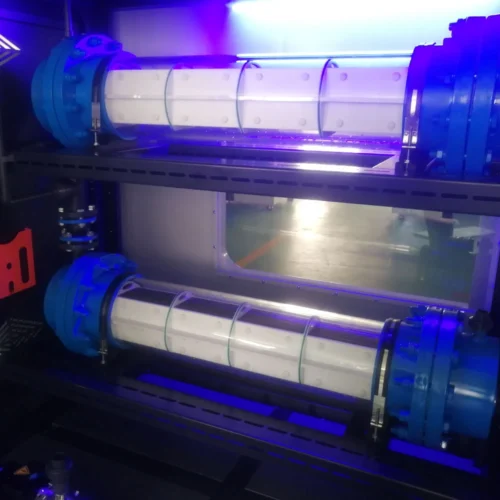
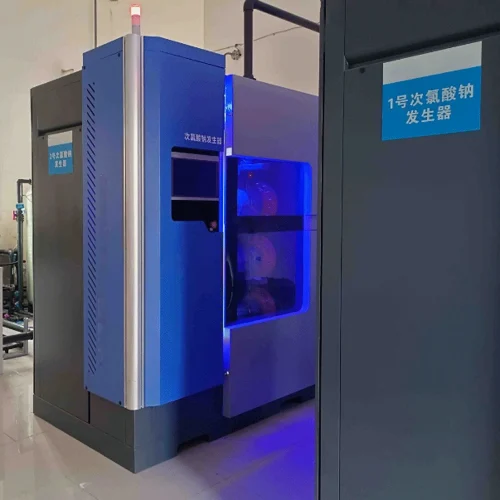
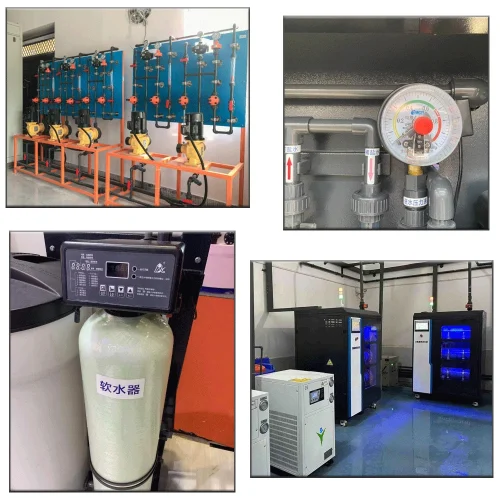
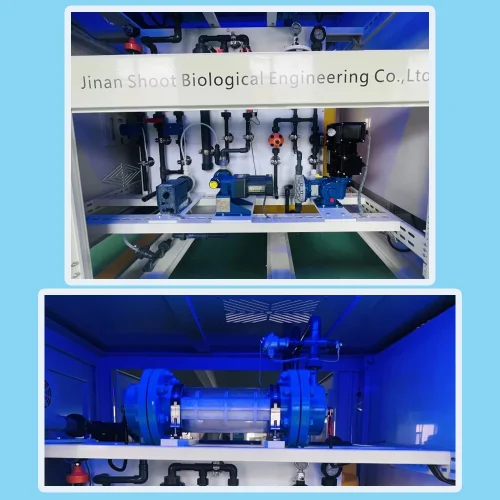
Forget complex engineering. Our system arrives pre-assembled and also pre-tested. The core components—the electrolytic cell, power supply, salt dissolver, and also dosing pump—are all housed in a single, compact unit. Installation is quick and straightforward. This significantly reduces project timelines and costs.
2. Real-Time Monitoring and Control from Anywhere.
This is the future of water management. The SHT-50G system features built-in IoT connectivity. Therefore, you can connect to it via a secure web portal or a dedicated mobile app. This gives you unparalleled control.
Monitor Key Parameters: Remotely view system status, chlorine production rate, salt levels, and also operational metrics on a clear dashboard.
Adjust Settings Instantly: Need to change the dosage? Simply adjust the setpoint from your computer or smartphone. No need to be on-site.
Receive Immediate Alerts: The system proactively sends automated alerts for any issues. Examples include low salt, low flow, or maintenance requirements. Meanwhile, this allows for proactive, not reactive, management.
3. Data-Driven Decision Making.
The system continuously logs all operational data. You can track usage trends, optimize chemical production, and also generate compliance reports effortlessly. This data is invaluable for improving efficiency and also demonstrating regulatory compliance.

4. Uncompromising Commitment to Safety
Safety is our highest priority. Every aspect of the PureGuard design focuses on protecting operators and the community at the same time.
1. Inherently Safer than Alternatives.
Producing low-concentration hypochlorite solution on-site eliminates the risks associated with transporting and also storing high-pressure chlorine gas or concentrated chemicals. There is no large-scale chemical inventory to manage at the same time.
2. Built-in Safety Protocols.
The system features multiple layers of protection:
Automatic Shutdown: Sensors detect failures and also immediately halt production.
Leak Detection: Integrated sensors monitor for any potential leaks.
Ventilation Monitoring: The cabinet monitors air flow to ensure safe operation at the same time.
3. Simple and Safe Operation.
The process is fully automated. Operator interaction is minimal. The system handles the entire process: brine mixing, electrolysis, and also dosing. This drastically reduces the potential for human error.

5. A Trusted Partner in Over 30 Countries

FAQ
1. Is on-site generation safer than liquid chlorine?
Yes! No toxic gas storage or transport risks. The system produces only what you need at the same time.
2. What’s the maintenance requirement?
Minimal. Regular cell cleaning and also salt refills. Automated alerts simplify upkeep.
3. How to handle maintenance?
Automated alerts guide servicing.
Factory advantage
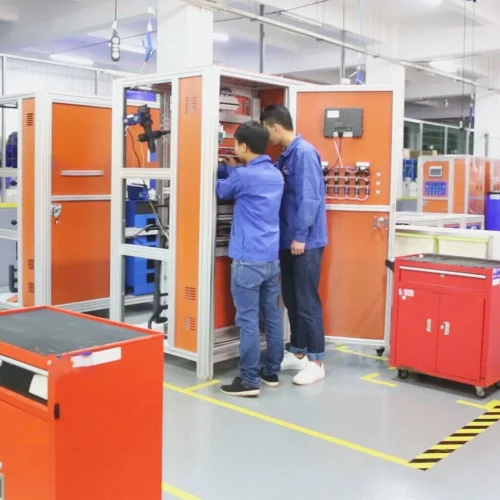
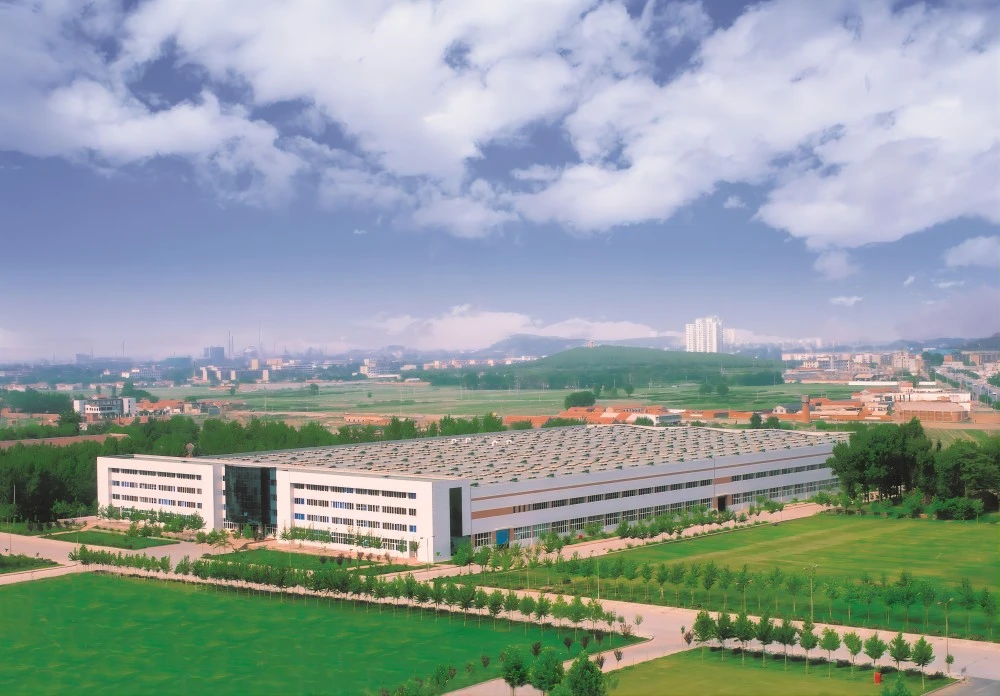
We have R&D centers, production centers, data centers and marketing centers. It is committe to providing technical support and innovative applications for improving public health security. Since its establishment, the company has obtained 12 invention patents and environmental management system certification. The company also has more than 30 test reports, covering surface and other different concentration detection projects. The series products sell well all over the country, and exported to such as Thailand, Malaysia, Cambodia, Brazil, South Africa, South America and other more than 20 countries and regions. The company has a perfect product sales and service system. To meet the needs of different customers with more professional services. So that to provide the best products and services for public health!
Customer feedback