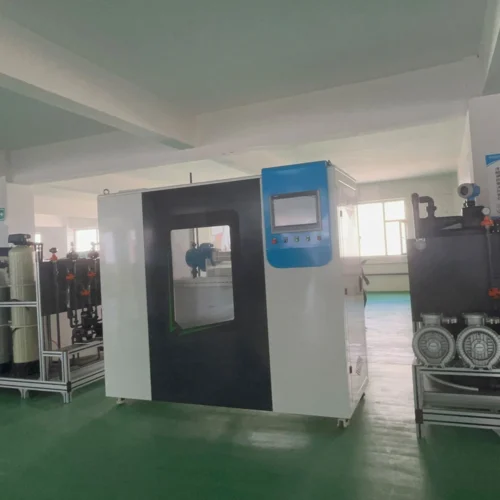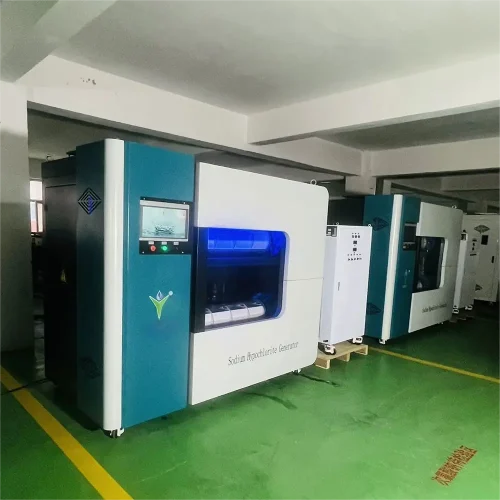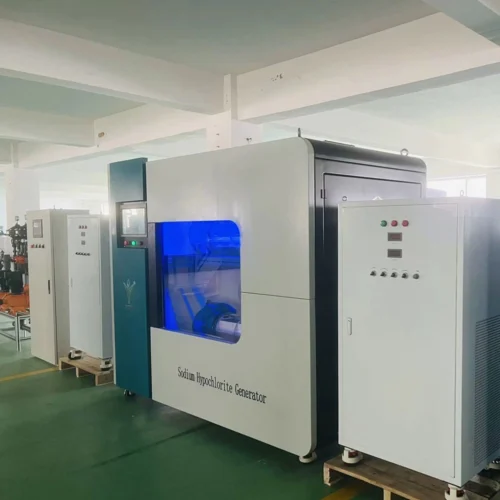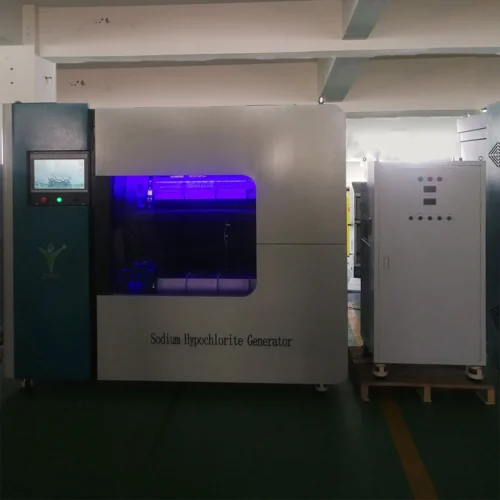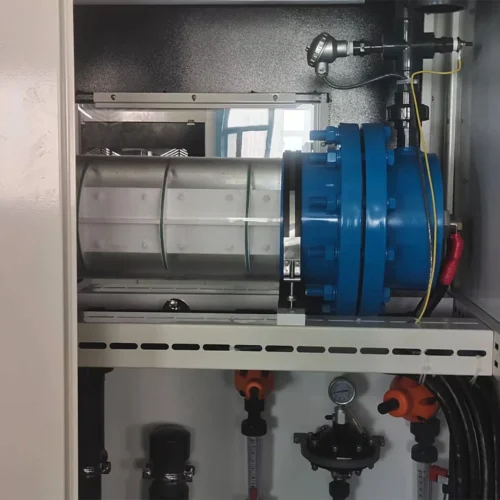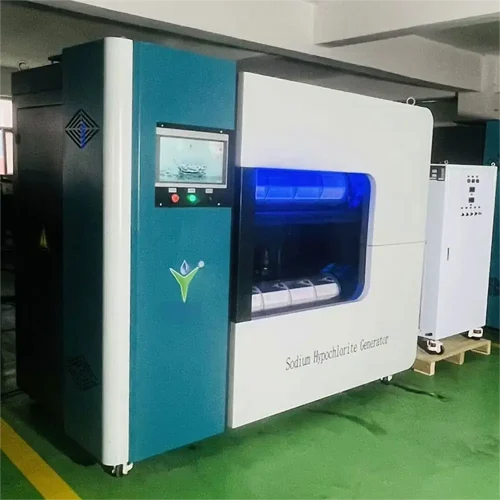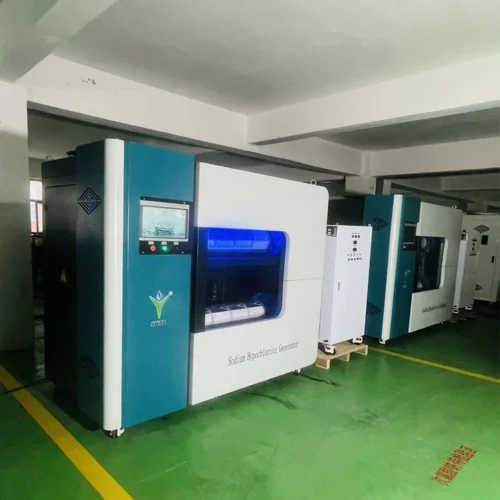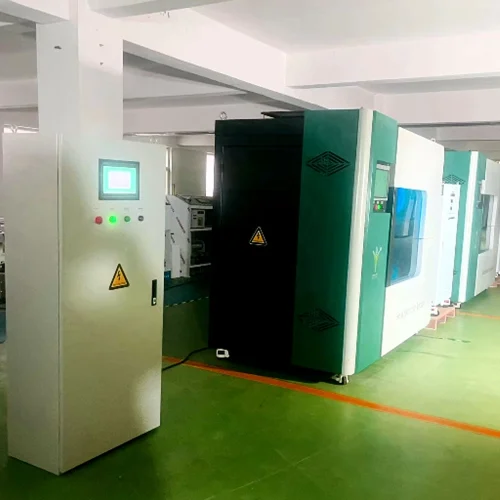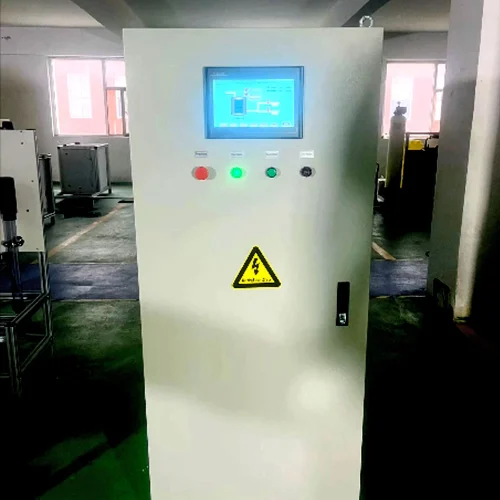


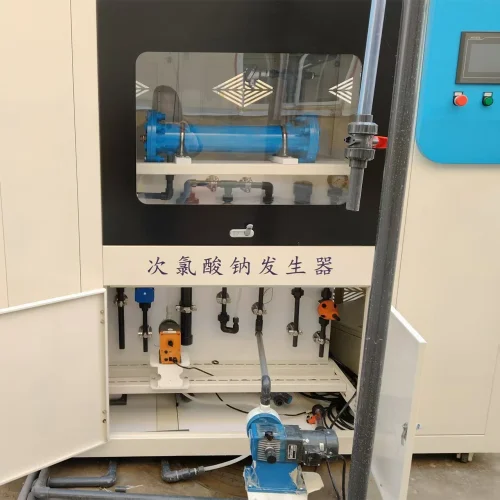
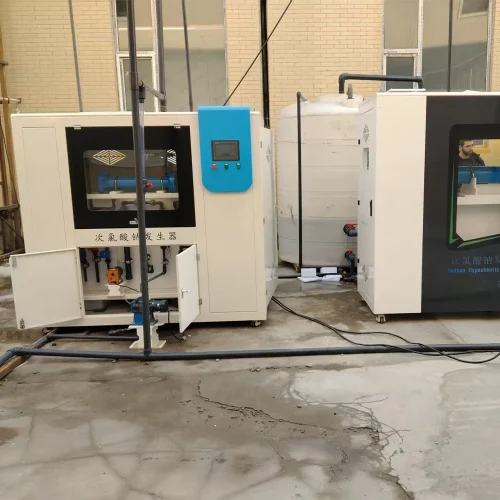
In the critical domain of municipal water treatment, the demand for reliable, cost-effective, and safe disinfection solutions has never been greater. Large-scale water treatment plants are the silent guardians of public health, tasked with delivering safe drinking water to burgeoning urban populations. Stepping up to this challenge is SHT-20000G, a state-of-the-art sodium hypochlorite generator designed to meet the rigorous demands of modern water purification facilities. This advanced system offers a paradigm shift from traditional chlorine gas and commercial hypochlorite solutions, championing on-site production for enhanced safety, operational efficiency, and long-term cost savings. With its robust 20,000 grams per hour production capacity, seamless network integration for automated operations, SHT-20000G is engineered to be the cornerstone of any large-scale water disinfection strategy.
1. The Imperative for Advanced Disinfection in Modern Water Treatment
Waterborne pathogens pose a constant threat to public health, making disinfection the most crucial step in the water treatment process. For decades, chlorine gas has been the disinfectant of choice. However, its transportation and storage present significant safety hazards, including the risk of catastrophic leaks. Consequently, many municipalities have transitioned to liquid sodium hypochlorite. While safer than gas, the transportation of bulk hypochlorite is costly, and the chemical degrades over time, leading to reduced efficacy and the formation of undesirable byproducts.
This is where SHT-20000G sodium hypochlorite generator excels. By producing sodium hypochlorite on-site, it eliminates the risks and inefficiencies associated with traditional methods. This forward-thinking approach not only enhances the safety profile of a water treatment plant but also provides greater control over the disinfection process. Furthermore, the ability to generate disinfectant on demand ensures a consistent and fresh supply, optimizing the treatment process for maximum efficacy.

2. Sodium hypochlorite generator parameter
| Product name | SHT-20000G |
|---|---|
| Effective chlorine yield | 20000g/H |
| Concentration | 6-8g/L(6000-8000ppm) |
| Power | 120KW |
| Salt consumption | 3.2KG/KG |
| Size | 2600*900*2000mm |
| Voltage | 380V/50hz |
3. Unveiling the Advantages of SHT-20000G
SHT-20000G is more than just a piece of equipment; it is a comprehensive solution that delivers a multitude of benefits to large-scale water treatment facilities. Its design and functionality are center around providing a superior alternative to conventional disinfection methods.
1. Enhanced Safety and Risk Mitigation
First and foremost, the on-site generation of sodium hypochlorite drastically reduces the safety risks associated with water disinfection. By producing a low-concentration (typically 0.8%) sodium hypochlorite solution, the SHT-20000G eliminates the need to transport and store hazardous, high-concentration chemicals. This mitigates the risk of accidental spills or leaks, safeguarding both plant personnel and the surrounding community. Moreover, the system operates at low pressures and temperatures, further enhancing its safety profile.
2. Significant Cost Reductions and Financial Viability
From a financial perspective, SHT-20000G presents a compelling case for long-term investment. The primary raw materials for the on-site generation process are salt, water, and electricity, all of which are readily available and significantly less expensive than purchasing bulk sodium hypochlorite. This leads to substantial operational cost savings over the lifespan of the equipment. Additionally, by eliminating the need for frequent chemical deliveries, transportation costs are eradicated, further contributing to a healthier bottom line. The initial capital investment in the SHT-20000G is often quickly offset by these ongoing operational savings.
3. Unparalleled Operational Efficiency and Automation
In an era of smart technology, SHT-20000G stands out with its advanced automation and network connectivity features. The system is designed for continuous and unattended operation, significantly reducing the need for manual intervention. Its network port allows for seamless integration into a plant’s Supervisory Control and Data Acquisition (SCADA) system. This enables operators to remotely monitor and control the generator’s performance, adjust production rates, and receive real-time alerts and diagnostics. This level of automation not only streamlines operations but also ensures a consistent and reliable supply of disinfectant, precisely matching the plant’s demand.
4. Superior Disinfectant Quality and Efficacy
The on-site generation process produces a fresh and highly active sodium hypochlorite solution. Unlike commercially produced hypochlorite, which can degrade during transportation and storage, the disinfectant generated by the SHT-20000G is at its peak efficacy. This freshness minimizes the formation of undesirable disinfection byproducts, such as chlorates and perchlorates, which can have adverse health effects. The consistent quality of the on-site generated hypochlorite ensures a more effective and reliable disinfection process, leading to superior water quality.
5. Environmental Responsibility and Sustainability
The adoption of SHT-20000G aligns with the growing global emphasis on environmental sustainability. By eliminating the transportation of hazardous chemicals, the carbon footprint associated with chemical deliveries is significantly reduced. Furthermore, the on-site generation process minimizes chemical waste and reduces the overall environmental impact of the water treatment process. This commitment to green technology not only benefits the environment but also enhances the public image of the water utility.

4. Applications of SHT-20000G in Large-Scale Water Treatment
The robust capacity and advanced features of SHT-20000G make it the ideal disinfection solution for a wide range of large-scale water treatment applications. Its versatility and reliability are unmatched in the industry.
1. Municipal Drinking Water Treatment Plants
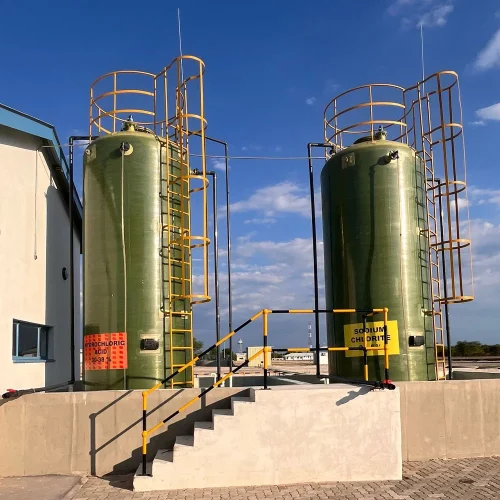
The primary application for the SHT-20000G is in large municipal drinking water treatment plants. With a production capacity of 20,000 grams of chlorine equivalent per hour, it can effectively disinfect vast quantities of water, ensuring that it is safe for public consumption. Its automated operation and remote monitoring capabilities make it a perfect fit for the complex and demanding environment of a modern waterworks.
2. Wastewater Treatment Facilities
Effective disinfection is also a critical final step in the wastewater treatment process to protect receiving water bodies. SHT-20000G can be seamlessly integrate into wastewater treatment plants to ensure that the treated effluent meets all regulatory standards before being discharge into the environment. Its reliable and cost-effective operation makes it an attractive alternative to traditional disinfection methods in this sector.
3. Industrial Water Treatment
Many industrial processes require large volumes of high-quality, disinfected water. The SHT-20000G can be utilized in a variety of industrial settings, including power plants, manufacturing facilities, and food and beverage processing plants, to ensure that the water used in their processes is free from harmful microorganisms. Its on-site generation capabilities provide a consistent and reliable supply of disinfectant, crucial for maintaining operational efficiency and product quality.
4. Cooling Tower Water Treatment
The growth of microorganisms in cooling towers can lead to biofouling, corrosion, and the proliferation of harmful bacteria such as Legionella. SHT-20000G provides an effective and automated solution for treating cooling tower water, preventing these issues and ensuring the safe and efficient operation of cooling systems.

5. A Trusted Partner in Over 30 Countries

FAQ
1. Is on-site generation safer than liquid chlorine?
Yes! No toxic gas storage or transport risks. The system produces only what you need at the same time.
2. What’s the maintenance requirement?
Minimal. Regular cell cleaning and also salt refills. Automated alerts simplify upkeep.
3. How to handle maintenance?
Automated alerts guide servicing.
Factory advantage
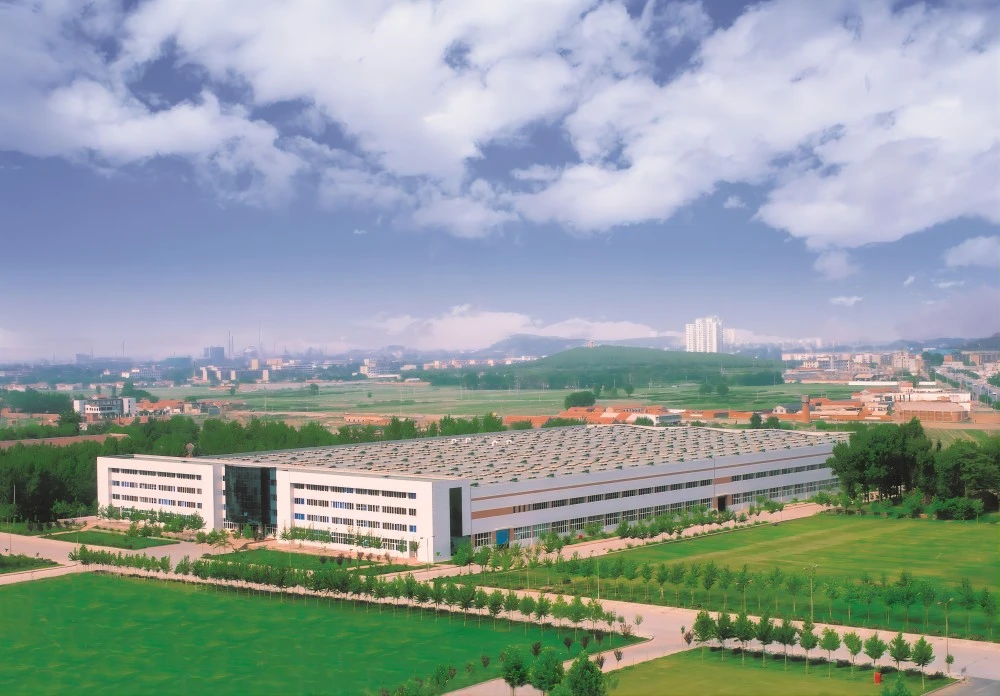
We have R&D centers, production centers, data centers and marketing centers. It is committe to providing technical support and innovative applications for improving public health security. Since its establishment, the company has obtained 12 invention patents and environmental management system certification. The company also has more than 30 test reports, covering surface and other different concentration detection projects. The series products sell well all over the country, and exported to such as Thailand, Malaysia, Cambodia, Brazil, South Africa, South America and other more than 20 countries and regions. The company has a perfect product sales and service system. To meet the needs of different customers with more professional services. So that to provide the best products and services for public health!
Customer feedback