
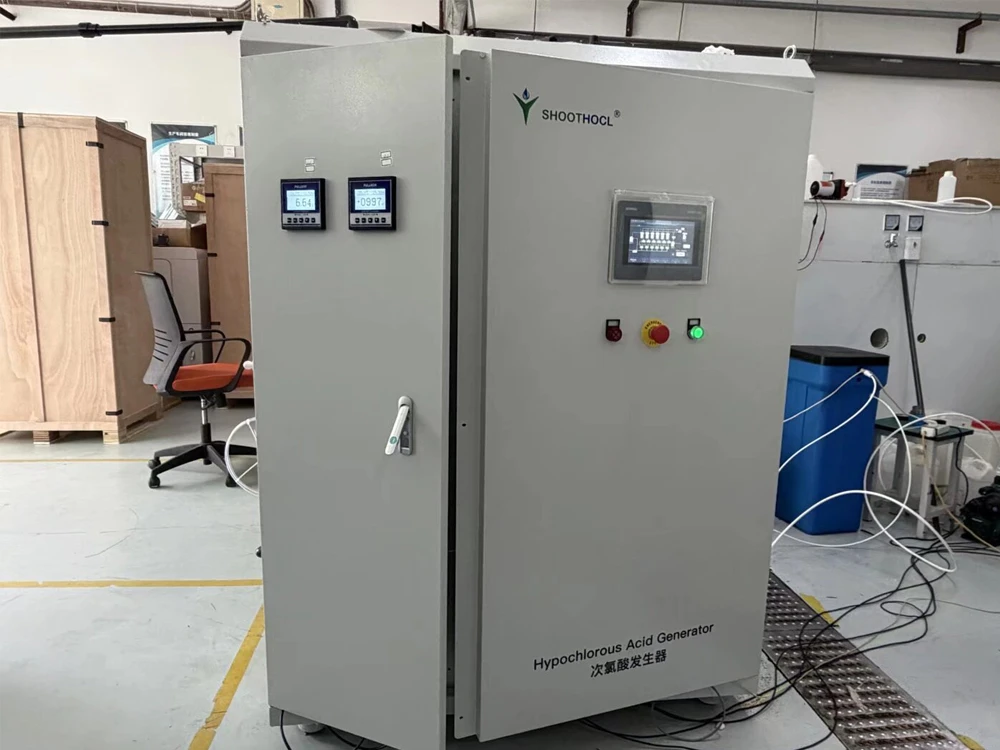
Food safety demands absolute precision, reliability, and efficiency. Our advanced Hypochlorous Acid (HOCl) Generator delivers a powerful, eco-friendly sanitizing solution tailored specifically for the food processing industry. By generating high-purity HOCl on-site, this system eliminates the need for harsh chemical storage while ensuring maximum hygiene.
We combine premium hardware, cutting-edge automation, and also an industry-leading service commitment. Here is how our product and service advantages transform your food safety operations.
Exceptional Product Advantages
We build our equipment for heavy-duty industrial environments. Every component focuses on durability, safety, and also consistent performance.
1. Market-Leading 30,000-Hour Warranty
Equipment downtime costs money, especially in the food industry. Therefore, we provide an extraordinary 30,000-hour warranty on our core electrolytic system.
This long lifespan translates to over three years of continuous, 24/7 operation.
We achieve this longevity through meticulous engineering and also premium materials.
You get predictable long-term operational costs and total peace of mind.
2. Premium Electrolytic Cell Technology
The electrolytic cell is the heart of any HOCl generator. We refuse to compromise on quality, so we use only top-tier components.
Premium Coating: Our cells feature robust titanium plates coated with a proprietary precious metal iridium-ruthenium alloy.
Stable Output: This advanced coating resists corrosion perfectly. It maintains highly stable available free chlorine (AFC) levels throughout its lifespan.
High Efficiency: The cell maximizes conversion rates. Consequently, it lowers salt and electricity consumption, saving you money every day.
3. PLC Intelligent Control System
Manual chemical mixing introduces human error. Our system replaces guesswork with absolute automation.
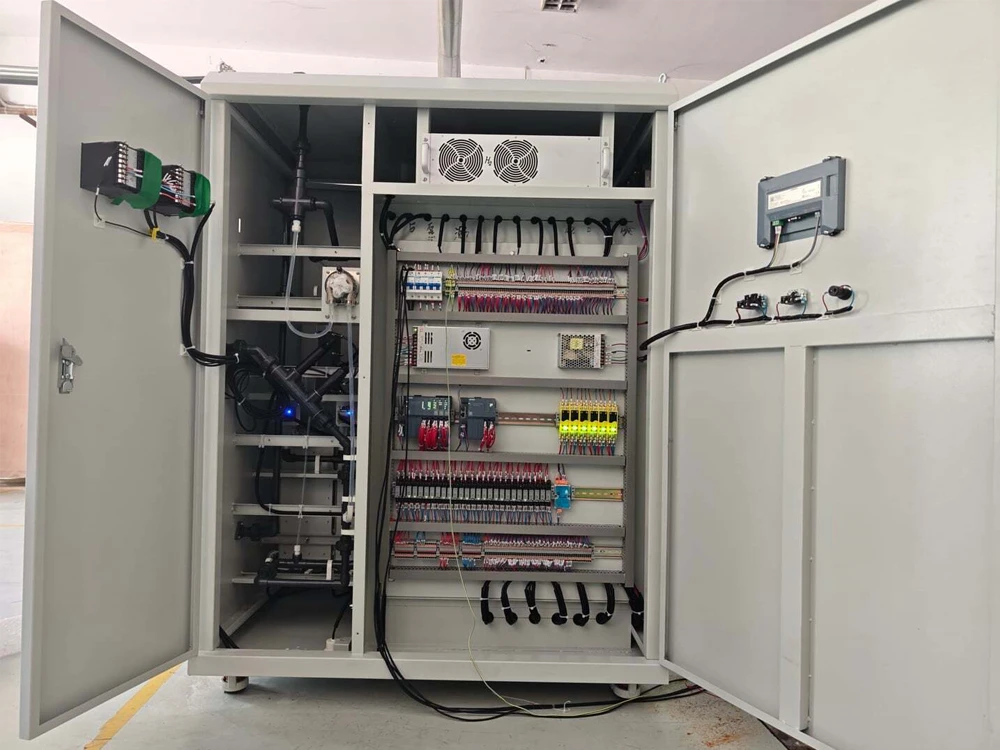
Siemens PLC Brain: A high-performance Programmable Logic Controller (PLC) manages the entire generation process.
Real-Time Monitoring: The system constantly tracks vital metrics. It monitors pH values, oxidation-reduction potential (ORP), and flow rates instantly.
Smart Alerts: If any parameter drifts, the PLC self-adjusts immediately. It triggers smart visual alerts before any drop in sanitizing quality occurs.
User-Friendly Interface: Operators navigate the system easily via a clear, responsive touchscreen dashboard.

Unmatched Service Advantages
Excellent hardware is only half of the equation. We support our technology with a comprehensive, customer-first service ecosystem at the same time.
1. Tailored System Engineering</strong>
Every food processing plant has unique layouts, water qualities, and also sanitizing demands. We never push a one-size-fits-all box.
Site Evaluation: Our engineers analyze your specific source water chemistry, water pressure, and also daily volume needs.
Custom Integration: We customize the generator setup to integrate seamlessly with your existing Clean-in-Place (CIP) systems, flume washers, or conveyor spray lines at the same time.
2. Proactive Technical Support
We protect your production timeline with rapid-response technical services.
Remote Diagnostics: Our PLC systems support secure remote connection modules. This allows our global tech team to troubleshoot software or diagnose issues within minutes, bypassing travel delays.
On-Site Experts: If you need physical assistance, our certified technicians deploy rapidly to minimize your operational disruptions.
Complete Training: We conduct thorough on-site training sessions for your operators. We cover routine maintenance, safety protocols, and software navigation.
3. Smart Lifecycle Maintenance
We help you stay ahead of maintenance schedules effortlessly.
Predictive Alerts: The intelligent control system monitors cell wear and runtime. It reminds your team precisely when to perform routine descaling or filter changes.
Reliable Parts Supply: We maintain a fully stocked inventory of genuine replacement parts, sensors, and also consumables to guarantee overnight shipping options.
Applications Across the Food Supply Chain
Our generator adapts beautifully to diverse food safety environments:
Produce Washing: Quickly eliminates foodborne pathogens like E. coli, Salmonella, and Listeria in vegetable flumes without damaging delicate leaves.
Meat & Poultry Processing: Sanitizes carcasses, processing tables, and cutting tools safely. It controls microbial loads effectively while extending product shelf life.
Seafood Preservation: Mixes easily into flake ice machines. This preserves freshly caught fish, controls strong odors, and prevents bacterial growth during transit.
Facility Sanitation: Disinfects large-scale floors, walls, and also hard surfaces rapidly through fogging or pressure spraying.

Upgrade Your Food Safety Standards
Do not let outdated chemical management or unreliable equipment jeopardize your brand reputation at the same time. Partner with us to secure a future-proof disinfection system. Contact our engineering team today to schedule your custom facility evaluation at the same time.
FAQ
How does the system achieve a 30,000-hour lifespan?
We use premium materials and smart engineering. The electrolytic cell utilizes thick titanium plates. We coat these plates with a highly stable, proprietary iridium-ruthenium precious metal alloy. Additionally, the PLC intelligent control system runs automated reverse-polarity cleaning cycles. This process prevents scale buildup and protects the coating from premature wear.